 English
 Español
 русский
 中文简体
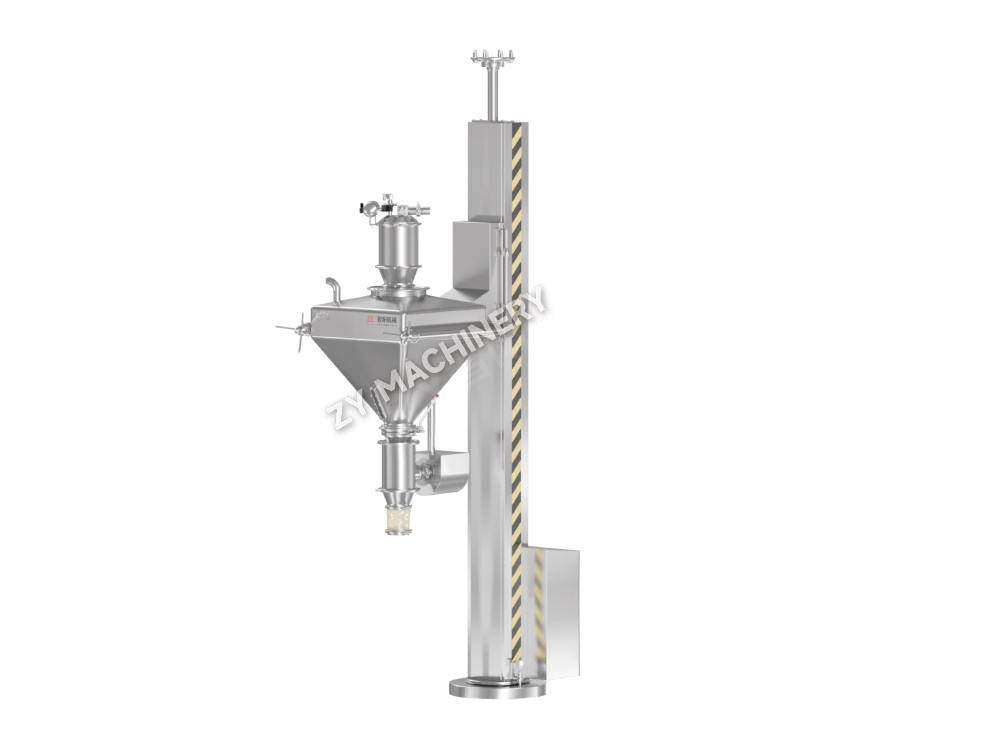
TLZ Dust-Free Feeding Station
The TLZ Dust-Free Feeding Station is designed to address dust generation du.....

Content
Accurate material dosing is one of the most important steps in pharmaceutical powder processing, oral solid dosage manufacturing, nutraceutical production, veterinary formulation, food processing, and other industries that depend on repeatable recipes. Even when mixing, granulation, drying, and coating equipment are highly advanced, the final product can be affected by inaccurate feeding at the beginning of the process. Variations in ingredient quantity may influence potency, flowability, content uniformity, bulk density, downstream processing behavior, and final product quality.
The LCP Weighing and Feeding Station is designed to address these challenges through an integrated system that combines dust-free material loading, vacuum conveying, temporary storage, screw feeding, precision weighing, and mobile material handling. Rather than treating weighing as an isolated operation, the system connects several process stages into a coordinated dosing platform. This approach helps manufacturers improve formulation accuracy, maintain a cleaner working environment, shorten batching cycles, and create a more controlled production workflow.
The equipment is suitable for production environments where several materials must be dosed according to a defined production order and formulation. Materials are introduced into an enclosed feeding station, transferred by vacuum to an elevated temporary storage silo, and then delivered by a controlled screw feeder into weighing hoppers mounted on an AGV mobile cart. The complete process is designed to reduce manual handling and limit dust exposure while maintaining accurate control over the quantity and feed rate of each material.
For manufacturers evaluating pharmaceutical powder processing equipment, the LCP system offers a combination of precision, flexibility, hygienic design, process integration, and intelligent control. Its value lies not only in the individual components but also in the way those components work together as a coordinated dosing solution.
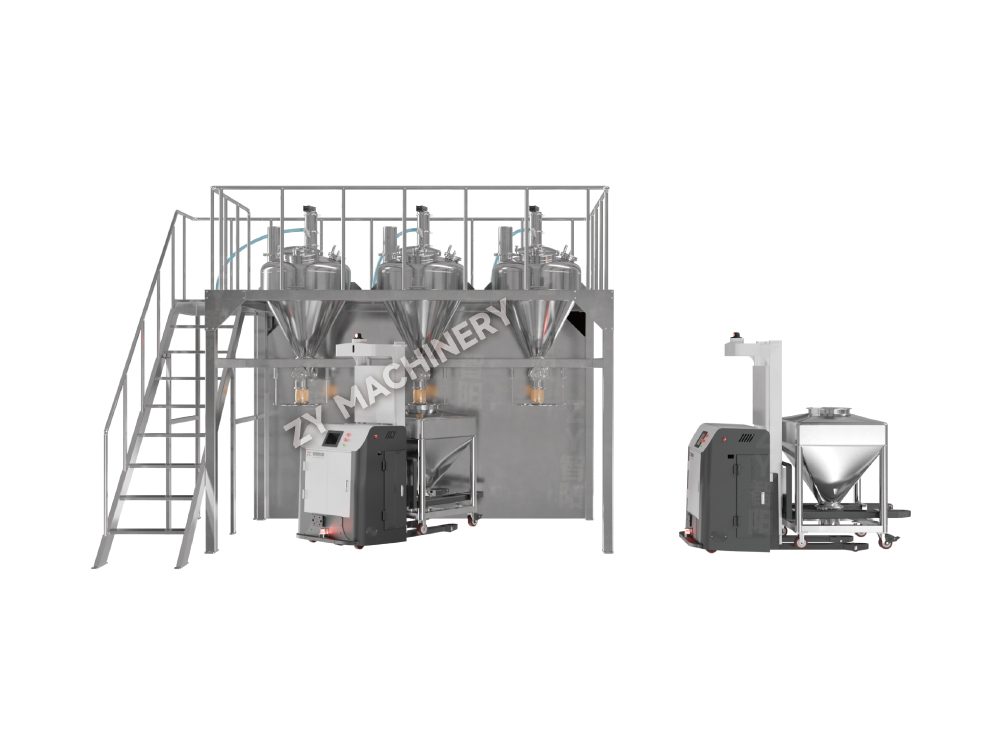
LCP Weighing and Feeding Station
Powder-based formulations often contain multiple ingredients with different physical characteristics. Some materials may be free-flowing, while others may be cohesive, light, electrostatic, hygroscopic, or sensitive to aeration. These differences create challenges during transfer and dosing. A system that handles all materials in exactly the same way may not provide stable performance across the complete formulation.
Accurate weighing is therefore more than a matter of placing material into a container and checking the final value. The complete feeding sequence must be controlled. Material must be transferred without unnecessary dust generation, stored temporarily without excessive segregation, and fed at a rate that allows the weighing system to reach its target accurately. The equipment must also support production operators in following the correct order and avoiding unnecessary waiting between batches.
In conventional operations, operators may manually lift bags or drums, open packages near the production area, transfer powder into containers, and weigh each material separately. This procedure can create several sources of variation:
First, manual handling may expose materials to the surrounding environment. This can increase the risk of dust release, cross-contamination, and operator exposure. Second, the accuracy of manual dosing may depend on individual operator practices. Third, separate weighing operations can increase the time required to prepare a batch. Finally, manually recording or transferring data may create opportunities for transcription errors.
The LCP Weighing and Feeding Station is intended to organize these activities into a more consistent process. By combining enclosed feeding, automated conveying, controlled screw delivery, and weighing hoppers, it provides a structured route from material input to formulation-ready output.
The working principle of the LCP system is based on the coordination of four primary functions: material feeding, vacuum conveying, temporary storage, and precision screw dosing into weighing hoppers. These functions are connected through an automated operating sequence so that materials can be delivered according to the production order and target formula.
The process begins at a dust-free feeding station. Materials are loaded into this enclosed area before being conveyed to the elevated temporary storage silo. Enclosing the input stage helps reduce powder escape during loading and supports a cleaner production environment. It also helps create a more organized interface between raw material handling and automated conveying.
The feeding station can be incorporated into a broader material management process in which operators identify, prepare, and load the required ingredients according to the batch instructions. By moving material loading into a defined location, the system helps separate raw material handling from later dosing operations.
After loading, a vacuum conveyor transfers the material toward the elevated temporary storage silo. Vacuum conveying is well suited to enclosed powder handling because the material moves through a controlled conveying route rather than being transported openly across the production area.
The enclosed route helps limit dust emission and reduces the number of manual transfer points. It can also support improved housekeeping and lower the risk of material loss during movement. For pharmaceutical and nutraceutical applications, these benefits are important because a controlled transfer path contributes to the overall hygiene strategy of the production line.
The temporary storage silo serves as an intermediate buffer between material transfer and final weighing. This buffer allows the conveying stage and the dosing stage to operate in a coordinated manner. The system does not need to depend on direct manual feeding into every weighing hopper, and material can be made available above the screw feeding mechanism for controlled delivery.
An elevated storage arrangement also supports gravity-assisted material flow toward the screw feeder. This design can help reduce unnecessary handling and provide a more stable supply condition for the dosing process. The temporary silo is especially useful when several materials must be prepared and delivered according to a defined sequence.
From the temporary storage position, the screw feeder delivers material into the weighing hoppers installed on an AGV mobile cart. Screw feeding provides controlled mechanical movement and enables the system to regulate the feed rate as the target weight is approached.
The weighing hopper receives the material and continuously monitors the accumulated quantity. The control system can use the weighing result and feed-rate information to manage the dosing operation. This arrangement supports accurate delivery while reducing the uncertainty associated with uncontrolled pouring or manual addition.
The weighing hoppers are mounted on an AGV mobile cart. This configuration gives the dosing system greater process flexibility because the weighed materials can be moved to the next manufacturing stage without requiring repeated manual transfer.
A mobile cart can also support different line layouts and production arrangements. Depending on the facility design, it may be positioned at the feeding and weighing area, then moved to a mixer, granulator, or another processing station. This creates a practical connection between weighing and downstream production while helping reduce intermediate handling.
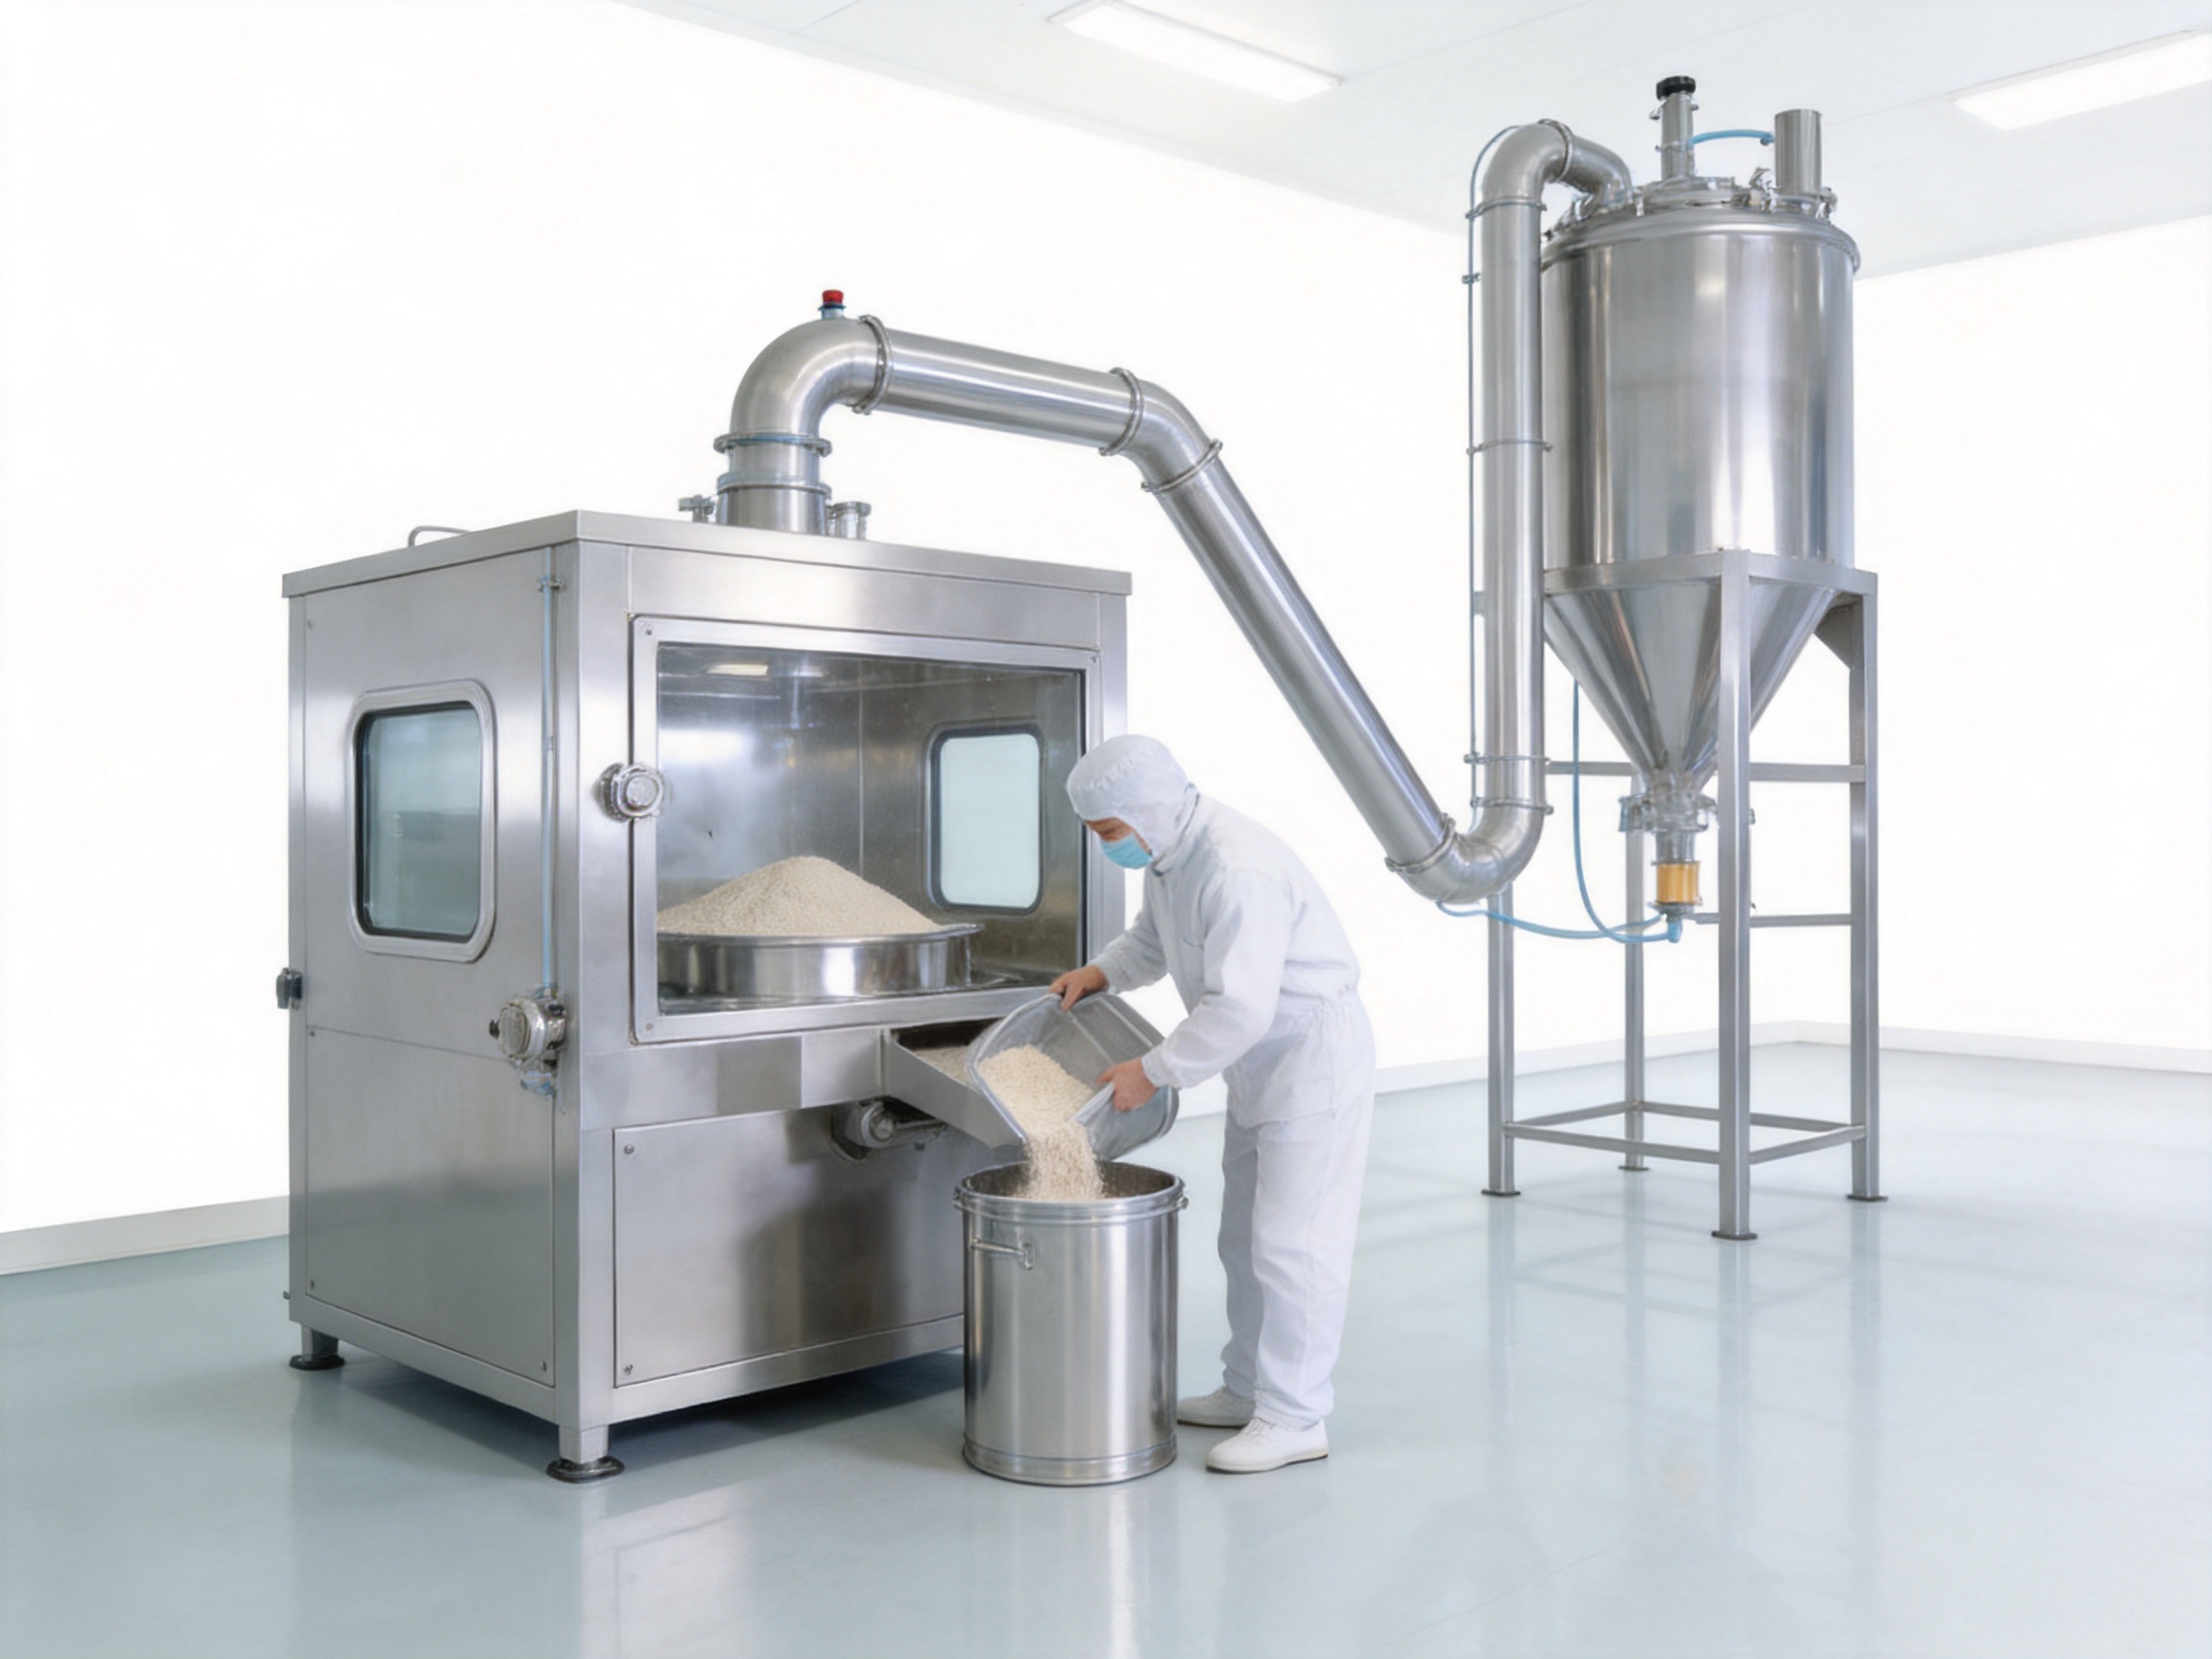
The system is designed to dose multiple materials according to production orders and formulation requirements. Its weighing and screw-feeding arrangement helps control the amount of each material instead of relying solely on manual estimation or batch-by-batch visual inspection.
Accurate dosing is particularly important when a formulation contains active ingredients, excipients, process aids, colorants, flavors, or other materials that must be added within a defined ratio. A controlled weighing procedure improves the consistency of each batch and can make downstream process results more predictable.
The stated accuracy class for the listed models is X(0.1). This specification indicates that the equipment is intended for high-accuracy weighing applications. Actual performance in operation will depend on material properties, installation conditions, calibration, feeding behavior, environmental factors, and the selected operating method. Nevertheless, the system architecture is designed to support repeatable and controlled measurement.
One of the key features of the equipment is its ability to support simultaneous operation of multiple weighing systems. This is valuable for formulations that require different materials to be dosed through separate weighing points or for production environments that need to prepare several materials within the same cycle.
Multiple weighing systems can reduce dependence on a single dosing point. If every material must pass through one weighing hopper in sequence, the overall batch time may increase. By supporting several weighing arrangements, the equipment can help distribute dosing work and improve the use of production time.
This capability also provides greater flexibility for different recipes. Some formulations may require relatively large quantities of a base powder, while others may involve smaller quantities of additives or active materials. Multiple weighing configurations allow the dosing strategy to be adapted to the process rather than forcing every material through an identical path.
The intelligent control system is designed to optimize feeding time and eliminate unnecessary waiting between hoppers. In a conventional manual process, one weighing operation may be delayed while an operator prepares the next container, confirms a material identity, or transfers a completed container to another location.
By coordinating the feeding, weighing, and movement functions, the system can support a more continuous batching cycle. This can shorten the time between material additions and improve equipment utilization. Faster batching does not simply mean increasing the screw speed. It means coordinating the complete sequence so that conveying, storage, weighing, and transfer support one another.
Intelligent control can also help operators follow a defined production order. A controlled sequence reduces the possibility of adding materials in the wrong order or leaving a required ingredient unprocessed. In regulated production environments, process sequence and batch traceability are important parts of manufacturing discipline.
The fully enclosed design helps prevent dust leakage during feeding, conveying, and dosing. Powder dust can affect equipment cleanliness, operator comfort, product quality, and maintenance requirements. In pharmaceutical manufacturing, uncontrolled dust may also increase the risk of cross-contamination and make cleaning more difficult.
By enclosing the main material route, the LCP system supports a cleaner production environment. The vacuum conveying route and enclosed feeding station reduce open powder transfer points, while the controlled screw feeder limits uncontrolled discharge. These features are especially valuable when handling fine powders or materials with poor flow characteristics.
A dust-reduced design also supports the implementation of good manufacturing practices. It does not replace the need for appropriate cleaning procedures, environmental control, validation, and operating discipline, but it provides a strong equipment foundation for those measures.
Production efficiency is influenced by more than the nominal capacity of a single machine. It also depends on preparation time, handling time, waiting time, cleaning effort, and the number of manual interventions. The LCP system addresses several of these factors within one integrated dosing process.
Automated conveying reduces repeated manual transport. Temporary storage makes material available for controlled feeding. Multiple weighing systems support parallel or coordinated operation. Intelligent controls help avoid idle intervals. Together, these functions can increase batching speed and improve overall production efficiency.
The listed capacity range for both stated models is 500 to 2,000 kilograms per hour. The actual capacity will depend on the material, recipe, bulk density, particle size distribution, moisture content, feeding behavior, target batch size, and operating sequence. Even so, the specified range demonstrates that the system is intended for more than small manual laboratory preparation and can serve industrial powder handling applications.
The available configurations include the LCP4-200/5 and LCP2-300 models. These models provide different weighing arrangements for production requirements involving different hopper quantities and capacities.
| Item | Unit or Description | LCP4-200/5 | LCP2-300 |
| Weighing system quantity | Number of systems | 4 | 2 |
| Weighing capacity | Hopper capacity | 200 kg and 5 kg | 300 kg |
| Accuracy class | Classification | X(0.1) | X(0.1) |
| Capacity | kg/h | 500–2,000 kg/h | 500–2,000 kg/h |
The LCP4-200/5 configuration is suited to operations requiring four weighing systems, including a combination of larger and smaller weighing capacity. The 200 kg and 5 kg arrangement can provide a practical balance between bulk material dosing and the controlled addition of smaller quantities.
The LCP2-300 configuration provides two weighing systems with a 300 kg weighing capacity. It may be appropriate for production processes that use larger quantities of fewer materials or that require a simpler weighing arrangement.
Model selection should be based on formulation structure, material characteristics, batch size, dosing sequence, required throughput, and facility layout. The most suitable system is not necessarily the one with the largest nominal capacity. A properly matched system can provide better accuracy, easier operation, and more efficient use of floor space.
A conventional weighing machine may measure material accurately, but it may not include the upstream feeding and conveying functions needed to deliver material in a clean and repeatable way. The LCP system combines weighing with material movement and temporary storage, creating a more complete process solution.
This integrated structure can reduce the number of separate machines and manual transfer points required around the weighing operation. It also allows the control logic to coordinate material availability, feeding rate, weighing status, and cart movement.
Manual powder handling is labor-intensive and can introduce variability. Operators may need to lift containers, transfer powders, clean spills, and move weighed materials between stations. The LCP system reduces these activities by using vacuum conveying and an AGV mobile cart.
Reducing manual intervention can improve workplace ergonomics and help operators focus on material identification, process monitoring, cleaning, and quality-related tasks. It can also support more consistent production when batch volumes increase.
Open transfer methods expose powder to the production environment and may create dust clouds during pouring, tipping, or scooping. The LCP system uses an enclosed feeding and conveying arrangement, which provides an important advantage for fine powder applications.
Improved dust control can reduce housekeeping requirements, protect nearby equipment, and support a more comfortable workplace. It can also help protect the material from environmental contamination during movement.
The availability of more than one model gives manufacturers options for different production needs. The system can be selected according to the number of weighing points, hopper capacity, throughput, and formulation structure.
This flexibility is useful for facilities that produce multiple products or operate across different batch sizes. Instead of applying a single fixed dosing method to every formulation, the manufacturer can select a configuration that corresponds more closely to actual production requirements.
The elevated temporary storage silo and mobile weighing cart help organize the vertical and horizontal movement of materials. A well-planned arrangement can reduce unnecessary floor-level storage and improve the connection between weighing and downstream processing equipment.
Because the cart can move between areas, the weighing station may support more than one process route. This can be useful in multiproduct facilities where different equipment trains operate at different times.
A major advantage of an integrated system is the ability to consider the complete process rather than only individual equipment specifications. Powder handling performance depends on the relationship between material properties, conveying conditions, storage design, screw geometry, weighing control, cleaning procedures, and downstream operations.
The equipment is developed for process integration, allowing the dosing solution to be considered as part of a larger line that may include mixing, granulation, drying, coating, transfer, and auxiliary processing. This process-oriented approach can help customers avoid compatibility problems between isolated machines.
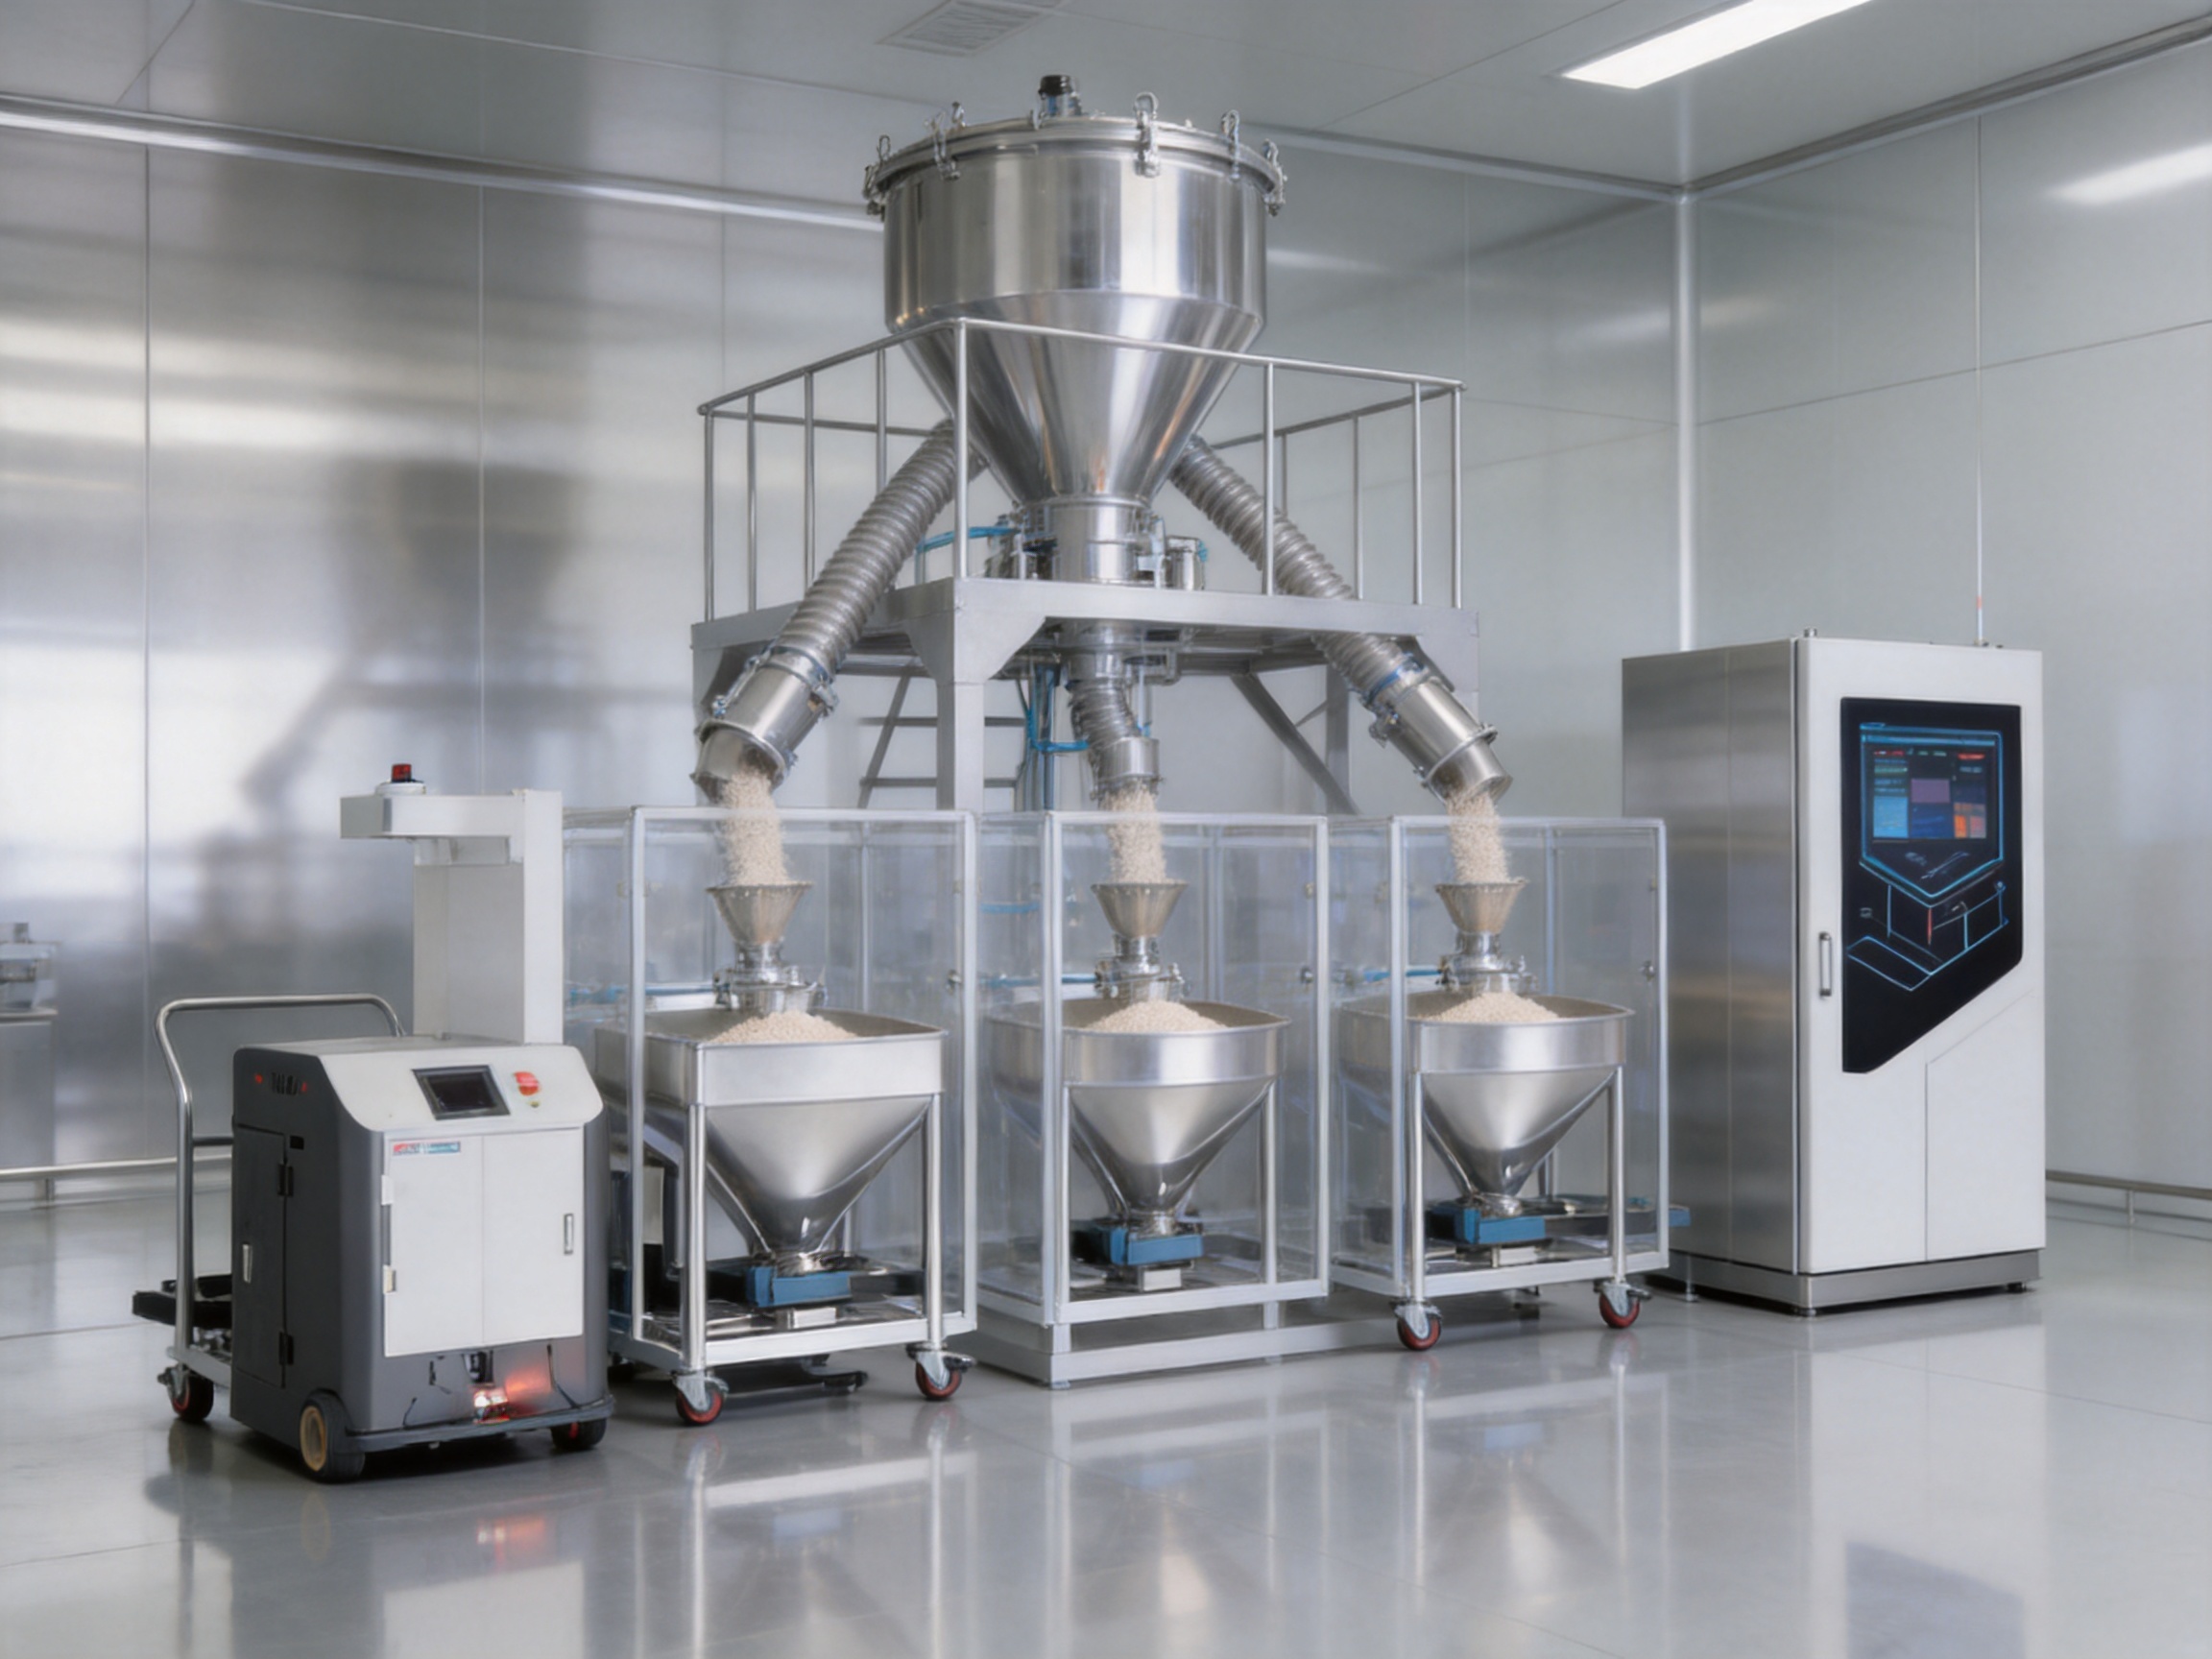
The manufacturer behind the LCP system specializes in the design, production, and process integration of powder processing and oral solid dosage equipment. Its product scope includes laboratory equipment, mixing equipment, granulation equipment, drying equipment, coating equipment, auxiliary processing equipment, and transfer and conveying systems.
This broad product range is important because a weighing and feeding station rarely operates independently in a pharmaceutical production line. It may need to supply a mixer, wet granulator, dry granulator, fluid bed dryer, tablet production process, coating system, or other downstream equipment. A manufacturer with experience across multiple process stages can better understand the interfaces between machines.
Different powders require different handling strategies. A material may bridge in a hopper, segregate during conveying, adhere to a screw, generate excessive dust, or behave inconsistently as moisture changes. Effective equipment design must consider these properties during the selection of conveying, storage, and feeding methods.
The manufacturer’s process-driven approach focuses on material characteristics, capacity requirements, and site conditions. This supports a more practical engineering process in which the equipment is matched to the application rather than selected only from a general-purpose catalog.
The company supplies standalone machines, modular systems, and complete production lines. This range allows a customer to begin with a specific dosing requirement and later connect the system to additional process equipment, or to develop a complete production solution from the beginning.
Modular equipment can be valuable when production capacity will expand over time. A facility may initially need a weighing and feeding station for one production line, then add additional systems, conveying routes, or downstream equipment as demand increases.
Continuous research and development are essential for powder processing equipment because material behavior, regulatory expectations, automation requirements, and production economics continue to change. The manufacturer has strengthened its research and development capabilities, developed patented technologies, and expanded its product portfolio over time.
Development work in this field may involve improving feeding stability, optimizing dust control, refining control systems, simplifying cleaning, improving equipment accessibility, and adapting designs to different production scales. These improvements can have a direct effect on reliability and total operating cost.
Reliable equipment requires controlled manufacturing processes. Material selection, fabrication, welding, surface treatment, component assembly, inspection, testing, and documentation all influence the final performance of a powder handling system.
The company has obtained quality system certification and emphasizes quality, reliability, and customer reputation. A quality-oriented manufacturing process helps ensure that the delivered equipment is consistent with the approved design and suitable for the intended production environment.
Every manufacturing site has different constraints. Available floor area, ceiling height, material routes, production room classification, cleaning access, electrical standards, utility connections, and downstream equipment locations can all affect the final system arrangement.
An equipment supplier that considers site conditions can provide a more practical solution than one that offers only fixed dimensions. The LCP station’s combination of elevated storage, mobile weighing, vacuum conveying, and modular process connections allows the system to be adapted to a variety of layouts.
The manufacturer has delivered equipment and engineering solutions to customers in multiple countries and regions. International project experience requires attention to documentation, communication, installation requirements, operator training, spare parts, and service support.
For customers purchasing pharmaceutical powder processing equipment from overseas, these capabilities are important. A successful project involves more than shipment of machinery. It also requires engineering coordination, commissioning support, operating guidance, and a clear understanding of the customer’s production objectives.
Pharmaceutical and nutraceutical facilities require equipment that supports hygienic operation and effective cleaning. The fully enclosed structure of the LCP station helps reduce dust release, while the controlled material route can reduce contamination opportunities associated with open handling.
GMP-oriented equipment design generally considers product-contact materials, surface condition, accessibility, dead zones, cleanability, drainage where applicable, inspection access, and separation of product and non-product areas. The final requirements depend on the application, material, facility classification, and validation strategy.
The LCP station should be evaluated as part of the customer’s complete hygiene and contamination-control program. The equipment can support a cleaner process, but operating procedures, cleaning validation, material identification, line clearance, environmental controls, and personnel practices remain essential.
For multiproduct facilities, the ability to reduce open transfer points is particularly valuable. Controlled movement can help minimize the spread of residual powder between work areas. Proper cleaning access and documented procedures should be incorporated into the project design from the beginning rather than added after installation.
In pharmaceutical production, the system can support the accurate dosing of active ingredients, excipients, binders, diluents, lubricants, and other formulation components. Its enclosed design and controlled weighing process are suitable for operations where dose accuracy and contamination control are important.
Tablet and capsule manufacturing depends on consistent formulation preparation. Before compression or encapsulation, materials may pass through mixing, granulation, drying, milling, and other stages. Accurate initial weighing helps create a consistent feed for these downstream operations.
Nutraceutical products often contain several powders, vitamins, minerals, botanical extracts, and functional ingredients. These materials may be required in different quantities and may have different flow properties. A flexible multi-weighing system can help improve preparation accuracy and production efficiency.
Veterinary formulations may require multiple active and carrier materials. Controlling the weighing and transfer process can support product consistency and reduce the risk of handling errors during batch preparation.
Industrial additives and specialty powders may also require enclosed transfer and accurate dosing. When materials are expensive, dusty, or sensitive to contamination, a controlled feeding route can help reduce material loss and improve operational control.
Before selecting a model, manufacturers should review the full production requirement rather than focusing only on hopper capacity. Important questions include the number of ingredients per batch, the required batch size, the target capacity, the proportion of large and small additions, and the sequence in which materials must be dosed.
Material testing may also be valuable. Bulk density, particle size, moisture, flowability, cohesion, electrostatic behavior, and sensitivity to aeration can all affect feeding performance. Testing helps determine whether changes to screw design, conveying conditions, hopper geometry, or control parameters are necessary.
The facility layout should be reviewed at the same time. The location of raw material loading, temporary storage, weighing, AGV movement, cleaning areas, and downstream processing equipment will influence the final system arrangement. Early layout planning can prevent later interference with personnel routes or maintenance access.
Customers should also define their expectations for automation, batch records, alarms, operator interfaces, recipe management, data collection, and connection with existing manufacturing control systems. These requirements can be addressed more effectively when discussed during the early engineering stage.
Correct installation is essential for weighing accuracy and stable feeding. The equipment should be positioned on a suitable foundation, leveled appropriately, and connected according to the required electrical and utility specifications. The weighing system should be protected from unnecessary vibration, airflow disturbance, and mechanical interference.
During commissioning, the conveying route, temporary storage silo, screw feeder, weighing hoppers, sensors, AGV movement, and control sequence should be tested together. Calibration and verification should be completed according to the customer’s quality procedures and applicable regulatory requirements.
Operators should be trained in material loading, recipe selection, start-up, shutdown, alarm handling, cleaning, and routine inspection. Training is especially important when the system operates with several weighing arrangements or when different formulas use different sequences.
Routine maintenance may include inspection of screw components, seals, sensors, filters, conveying lines, hopper surfaces, mobile cart wheels, electrical connections, and safety devices. Preventive maintenance helps identify wear before it affects dosing accuracy or production continuity.
Cleaning procedures should be designed around the material properties and product changeover requirements. Operators should have clear instructions for opening access points, removing residual powder, inspecting contact surfaces, and confirming line clearance before the next batch.
The economic value of a weighing and feeding station should be assessed across the complete production lifecycle. The purchase price is only one part of the investment. Labor requirements, material loss, cleaning time, production delays, batch deviations, maintenance, and future expansion also influence the total cost of ownership.
By automating material transfer and reducing manual weighing activities, the LCP system can help lower labor intensity. Its enclosed design may reduce housekeeping work and improve the efficiency of cleaning operations. Intelligent control and multiple weighing systems can shorten batching cycles, allowing production assets to be used more effectively.
Accurate dosing also protects the value of raw materials. Overdosing can increase material costs, while underdosing or incorrect formulation may lead to batch rejection or reprocessing. A reliable weighing process supports better control of both product quality and material consumption.
The mobile cart can provide additional operational value by connecting the dosing station to different downstream process areas. This flexibility may reduce the need for fixed transfer equipment in every location and support a more adaptable factory layout.
Powder processing is a chain of connected operations. The behavior of material during weighing can influence conveying. Conveying conditions can influence segregation. Storage can influence flow. Feeding can influence the final formulation ratio. The completed batch can then influence mixing, granulation, drying, and coating performance.
For this reason, a dosing station should be selected with consideration for the complete production route. A technically accurate weighing system may still create problems if the material enters the next stage in an unsuitable condition or if the transfer process causes excessive segregation.
An integrated engineering approach helps address these relationships. The equipment supplier can evaluate the material route, production sequence, required capacity, available space, downstream interfaces, and cleaning strategy together. This can reduce the risk of purchasing equipment that performs well in isolation but does not fit the complete manufacturing process.
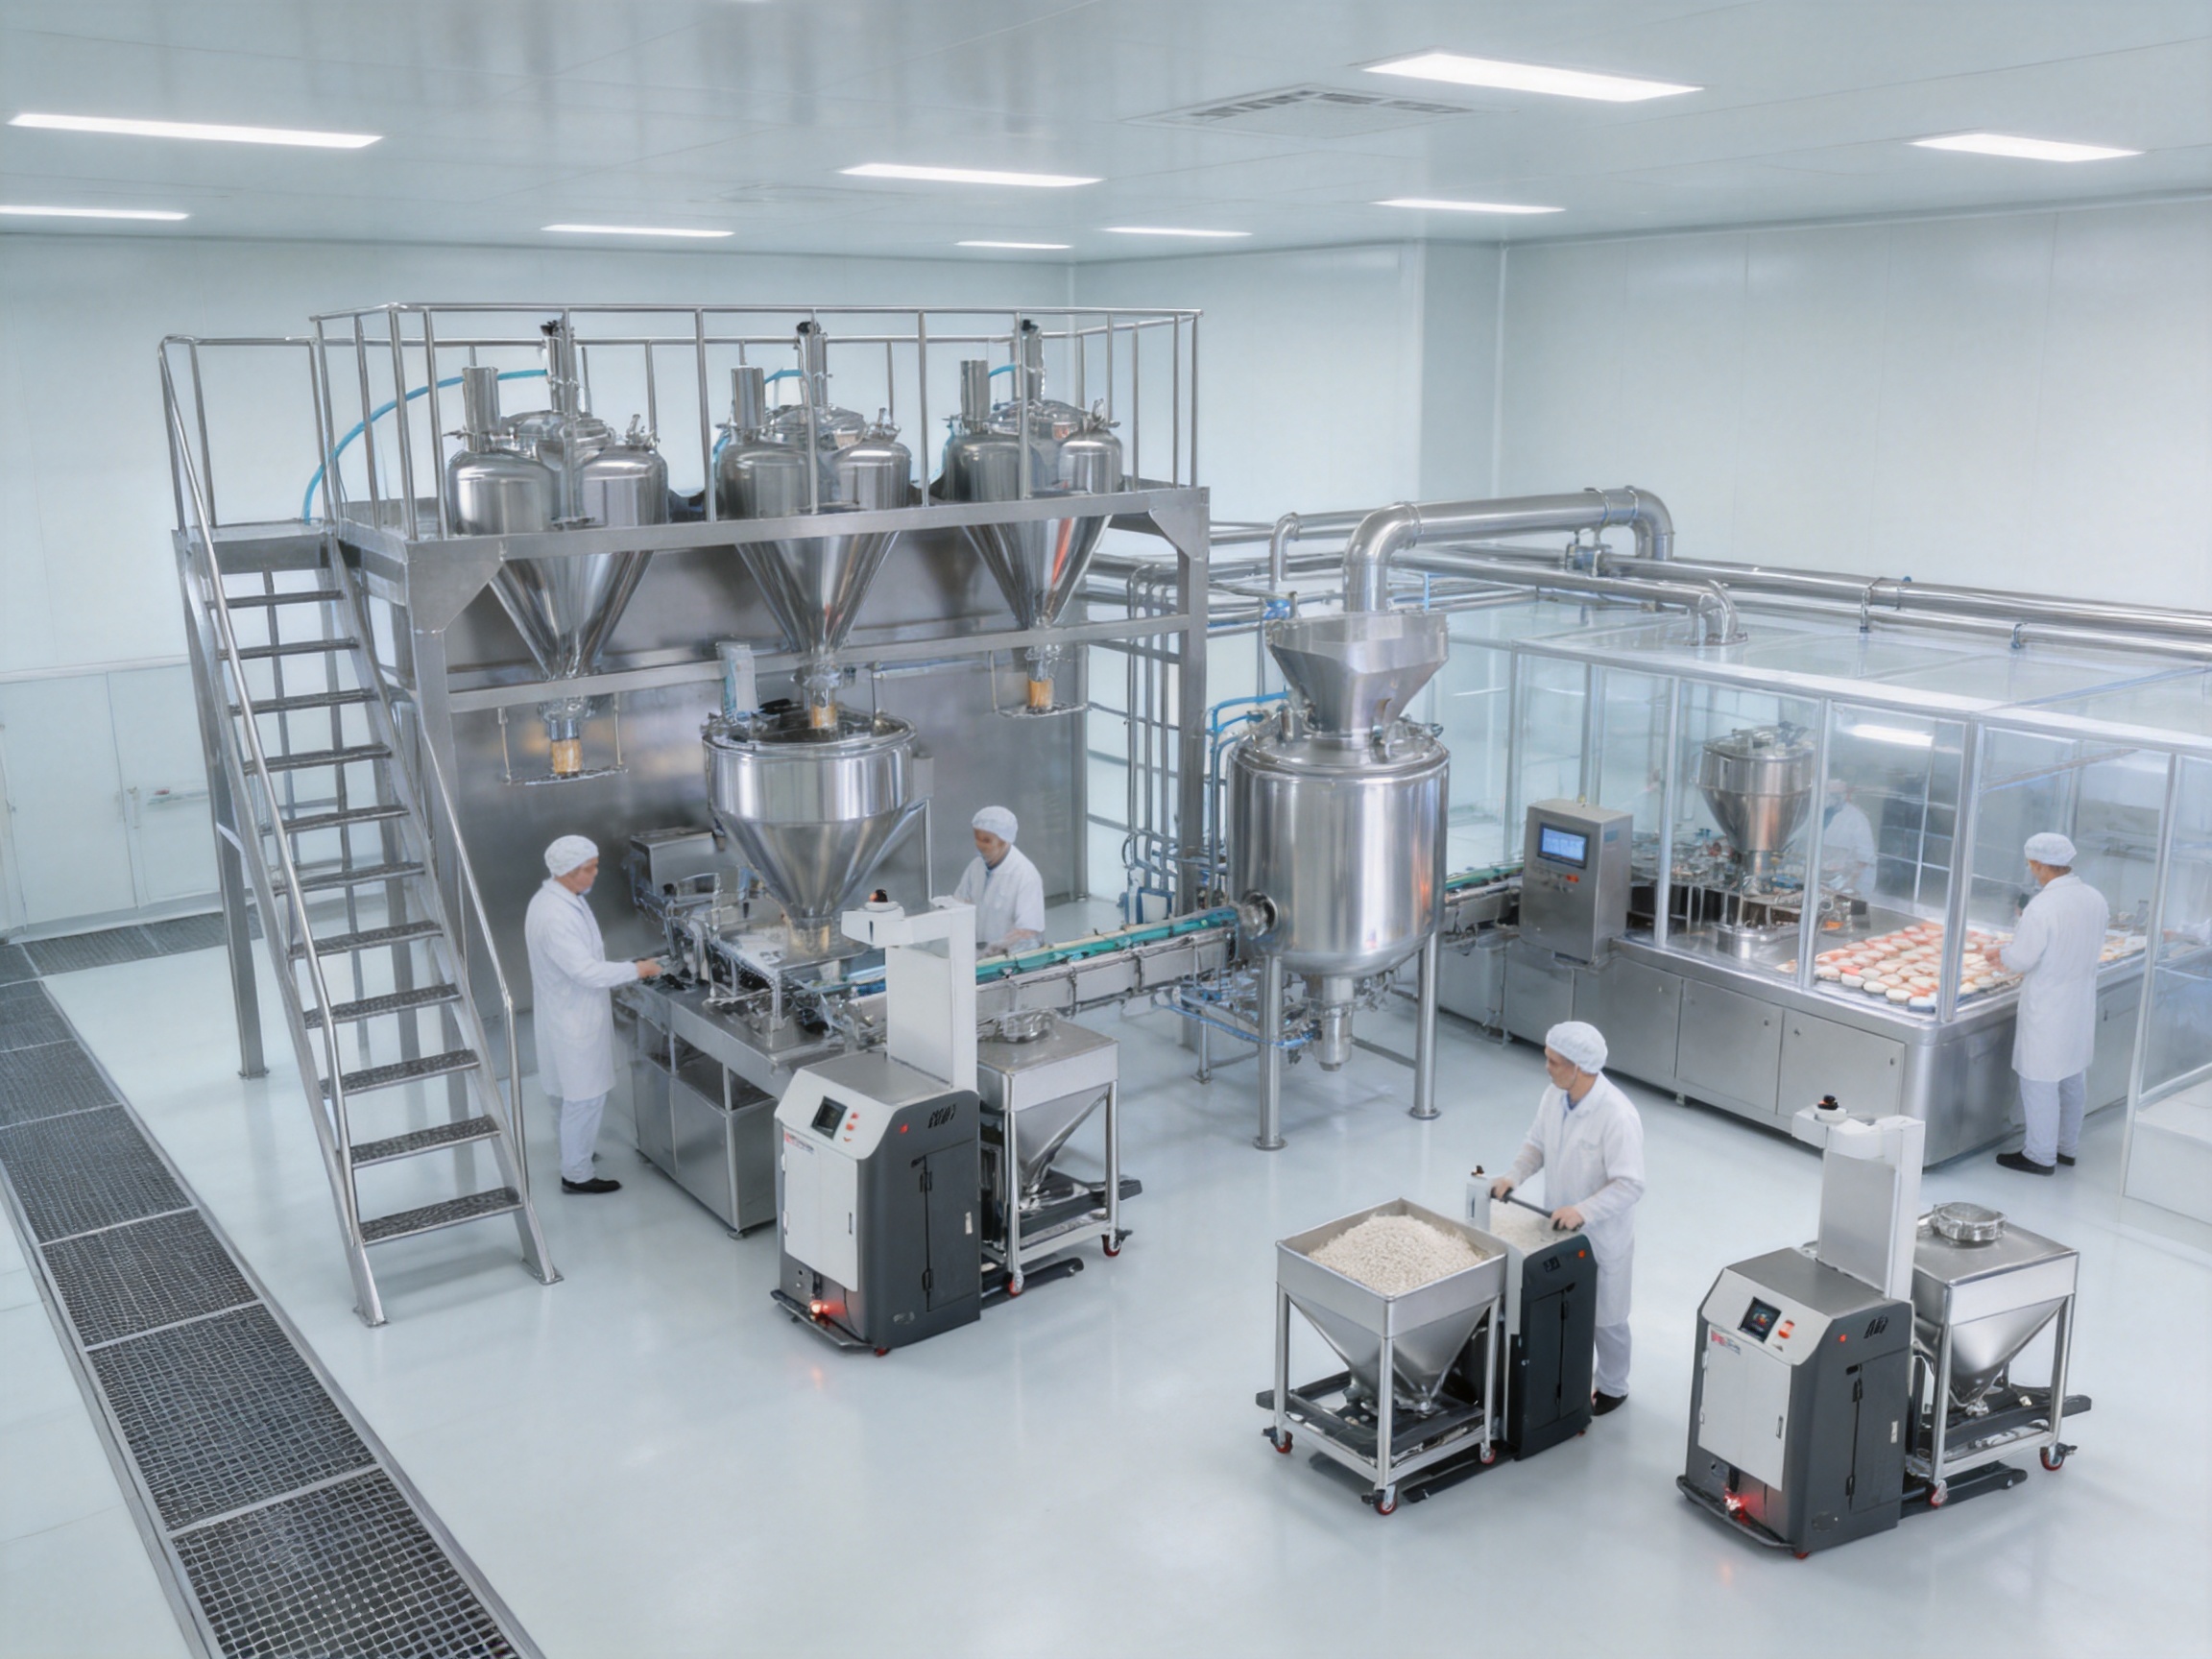
The main purpose is to accurately dose multiple materials according to production orders and formulation requirements. The system combines enclosed feeding, vacuum conveying, temporary storage, screw feeding, weighing hoppers, and mobile material handling.
Materials are loaded into a dust-free feeding station and transferred through an enclosed vacuum conveying route. The temporary storage and screw-feeding stages are also integrated into the controlled material path, reducing open powder transfer and potential dust leakage.
Yes. The system is designed for multi-material dosing and supports multiple weighing systems. The exact number of weighing systems and their capacity depend on the selected model and production requirements.
The listed models are LCP4-200/5 and LCP2-300. The first model provides four weighing systems with a 200 kg and 5 kg combination, while the second provides two weighing systems with a 300 kg capacity. Both are listed with an X(0.1) accuracy class and a capacity range of 500 to 2,000 kilograms per hour.
The temporary storage silo acts as a buffer between vacuum conveying and final dosing. It keeps material available for the screw feeder and helps coordinate the transfer stage with the weighing stage.
A screw feeder provides controlled mechanical delivery of material into the weighing hopper. It can regulate the feed rate and help achieve the target weight more accurately than uncontrolled pouring or manual addition.
The mobile cart allows weighed materials to be moved to the next process area with less manual handling. It can also provide greater flexibility for different production layouts and connections with downstream equipment.
The fully enclosed and dust-reduced design supports a cleaner, GMP-oriented production environment. However, final suitability depends on the complete equipment specification, installation, cleaning procedures, validation requirements, facility design, and applicable regulations.
Selection should consider the number of materials, batch size, required capacity, weighing accuracy, proportion of large and small additions, available space, and the required production sequence. Material testing and process engineering review are recommended before final selection.
Yes. The system is intended to operate as part of a broader powder processing workflow and can be considered alongside mixing, granulation, drying, coating, auxiliary processing, and transfer equipment.
Actual capacity depends on material density, particle size, moisture content, flowability, cohesion, formula structure, target weight, screw configuration, conveying distance, and operating sequence. The published range is a reference for the stated configurations, while final performance should be confirmed for the specific application.
No. Automation reduces repetitive handling but operators remain responsible for material identification, loading, process supervision, cleaning, maintenance checks, alarm response, and compliance with production procedures.
The LCP Weighing and Feeding Station provides an integrated approach to accurate powder dosing. By combining dust-free feeding, vacuum conveying, elevated temporary storage, controlled screw delivery, precision weighing, and AGV-based movement, it addresses several common weaknesses of manual and disconnected dosing operations.
Its principal advantages include multi-material dosing, support for multiple weighing systems, intelligent control, reduced waiting time, enclosed powder handling, improved batching efficiency, and flexible connection with downstream processes. The available models provide different weighing arrangements for varying production requirements, while the listed accuracy class and throughput range demonstrate the system’s suitability for industrial powder processing applications.
The equipment is strengthened by a process-oriented manufacturing approach that considers material characteristics, capacity, site conditions, and complete-line integration. The manufacturer’s experience across laboratory, mixing, granulation, drying, coating, conveying, and auxiliary equipment allows the dosing station to be considered as part of a broader production solution rather than as an isolated machine.
For pharmaceutical, nutraceutical, veterinary, additive, and related powder-processing facilities, reliable weighing is the foundation of consistent formulation preparation. A well-designed automated station can help improve accuracy, cleanliness, production speed, operator safety, and long-term process control. When properly selected, installed, validated, and maintained, the LCP system can become an important component of an efficient and modern powder processing line.
1. Product information supplied for the LCP Weighing and Feeding Station, including operating principle, features, models, and technical parameters.
2. General principles of pharmaceutical powder handling, material transfer, weighing, and formulation control.
3. Good manufacturing practice principles relating to equipment hygiene, contamination control, cleaning, and process documentation.
4. General engineering practices for vacuum conveying, screw feeding, weighing systems, temporary storage, and automated material handling.
5. General guidance for process integration in oral solid dosage and powder-based manufacturing systems.
Want to stay up to date?
Contact us via the email address below.
Don't worry about spam. We hate it too!
Mobile Client
Video Account
Phone:+86-15161130178
Tel:+86-519-88674267
Email:czzy188@163.com
Phone:+86-15161132798
Email:zy@zy-drying.com
WeChat ID
Copyright 2026 Changzhou Zhiyang Machinery Equipment Co., Ltd. All Rights Reserved  Oral Solid Dosage Equipment Manufacturer