 English
 Español
 русский
 中文简体
GFH R&D High-Containment Solid Dosage Production Line
The GFH R&D High-Containment Solid Dosage Production Line is designed f.....

Content
The development and manufacture of highly potent pharmaceutical products require more than a conventional granulator, dryer, mixer, or tablet-processing machine. When materials include anticancer compounds, highly sensitizing substances, or other hazardous active pharmaceutical ingredients, the production system must protect operators, preserve product quality, prevent cross-contamination, and maintain reliable process control from material charging through final discharge.
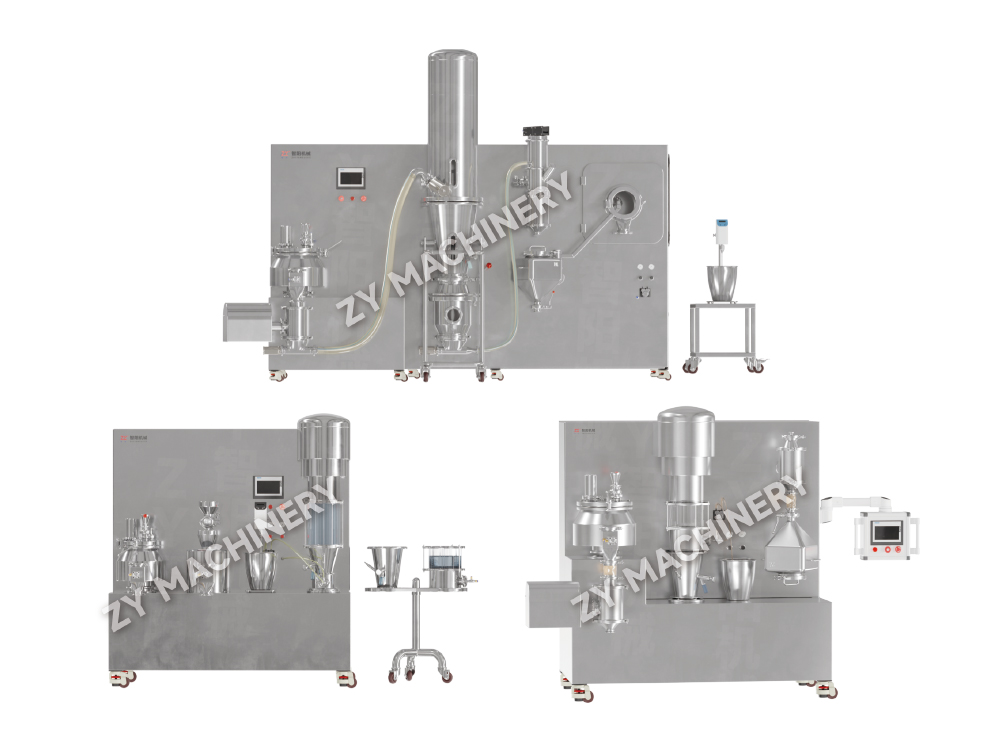
The GFH R&D High-Containment Solid Dosage Production Line is designed for this demanding environment. It integrates containment technology with wet granulation, fluidized-bed drying, dry granulation, mixing, conveying, and controlled discharge. The result is a compact and adaptable process platform for the research, development, pilot-scale, and small-batch production of tablets, capsules, and other oral solid dosage forms.
Unlike a collection of independent machines connected by open transfers, the system is designed around a continuous contained process route. Raw materials enter through a Rapid Transfer Port, or RTP, and remain within a controlled isolator environment as they pass through granulation, drying, milling or dry granulation, mixing, and discharge. This integrated approach helps reduce operator exposure, minimize material loss, improve process repeatability, and simplify the management of potent powders.
Oral solid dosage manufacturing commonly involves powders, granules, and intermediate products that can become airborne during charging, discharging, sampling, blending, or transfer. In conventional production environments, these operations may create exposure risks for operators and maintenance personnel. Even when the quantity of active ingredient is small, a highly potent compound can require strict engineering controls.
Containment is particularly important for anticancer drugs, hormones, sensitizing compounds, immunosuppressive materials, and other substances with occupational exposure limits that demand specialized handling. A high-containment process must address not only the main production step but also every point where material could escape, including door openings, filter changes, glove ports, transfer connections, equipment interfaces, waste removal, and final product discharge.
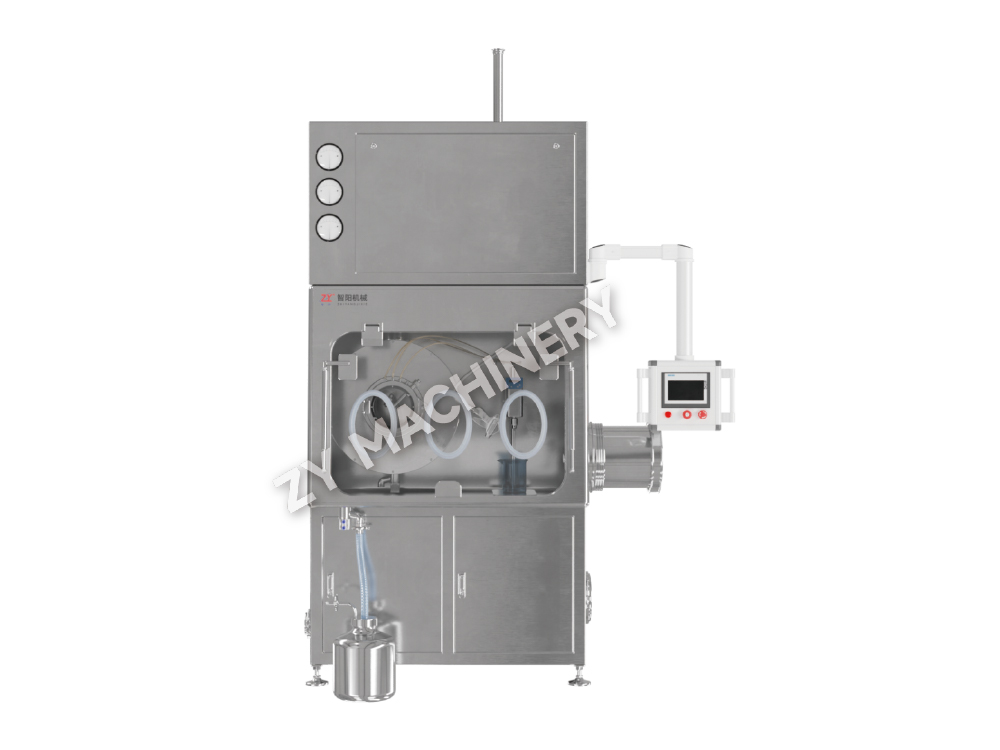
The GFH system addresses these concerns by placing the principal processing route inside an isolator. The isolator provides a physical barrier between the product and the surrounding workplace. Operators can perform necessary tasks through glove ports, half-suits, or optional robotic systems, while the ventilation and filtration arrangement maintains controlled airflow and negative pressure during normal operation.
Containment also supports product quality. An enclosed system reduces the opportunity for foreign particles, environmental moisture, or unrelated materials to enter the process. It can also reduce cross-contamination between products when appropriate cleaning, validation, and changeover procedures are implemented.
The production line is designed to provide a logical process sequence for high-containment solid dosage development. Materials are introduced through an RTP valve and then transferred to a wet granulation vessel. After granule formation, the wet material is moved by vacuum to a fluidized-bed drying unit. The dried material proceeds through discharge and dry granulation operations before entering a mixing hopper. Once the final blending operation is complete, the finished granules are discharged through AB valves.
Each stage is connected through a controlled transfer strategy rather than relying on open manual handling. This reduces the number of exposed interfaces and supports a more consistent material path. It also enables the equipment configuration to be adapted to different formulations, batch sizes, and research objectives.
The process begins with the controlled transfer of raw materials into the isolator. An RTP valve provides a secure interface between the external material container and the internal processing area. The transfer connection is designed to limit direct exposure during loading and to help maintain the integrity of the containment boundary.
RTP systems are especially useful in potent-product development because they offer a repeatable transfer method. Instead of manually opening bags or containers inside an uncontrolled environment, operators can use a dedicated port and compatible transfer device. The exact transfer container, connection format, and operating procedure can be selected according to the project requirements.
The system may also be configured with transfer chambers or sleeve systems. Interlocked chamber doors help prevent both sides of a transfer chamber from being opened simultaneously, supporting safer material movement and reducing the risk of accidental loss of containment.
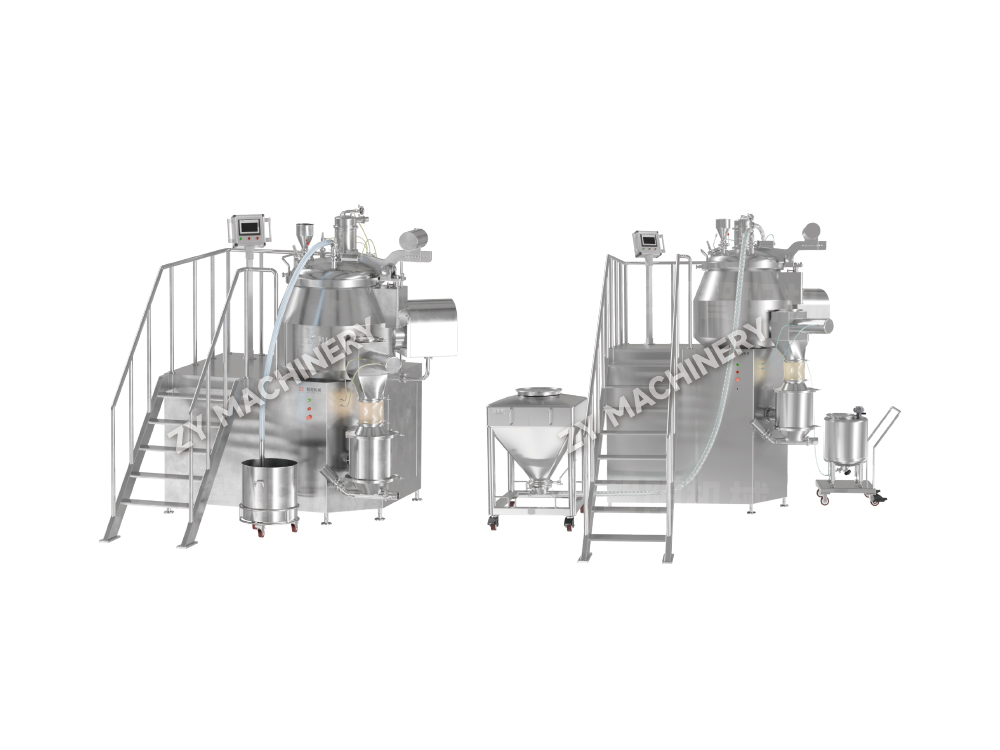
After charging, the materials are fed into the wet granulation vessel. Wet granulation is widely used to improve powder flow, compressibility, particle-size distribution, and handling characteristics. In a research and development environment, the ability to control granulation conditions is important because relatively small changes in binder addition, mixing time, impeller speed, or endpoint can affect the final tablet or capsule performance.
Within a high-containment line, the granulation vessel must function as both a process machine and a contained enclosure. The equipment arrangement helps prevent the release of dust during charging, wet massing, and discharge. A suitable design can also support controlled addition of liquid binders, formulation observation through protected interfaces, and process adjustments through the control system.
Integrating wet granulation into the contained process route offers an advantage over isolated equipment that requires manual transfer. The product does not need to be removed from the isolator and carried to a separate open machine. This reduces handling steps and helps maintain a consistent level of protection during one of the most dust-sensitive stages of production.
Following wet granulation, the wet granules are conveyed to the fluidized bed by vacuum transfer. Vacuum conveying minimizes manual handling and provides a controlled route between the granulation vessel and drying equipment. The transfer system can be selected or adjusted according to the material’s density, moisture content, particle size, and flow behavior.
Fluidized-bed drying uses a controlled airflow to suspend and dry the wet granules. The drying process can improve moisture uniformity and reduce the time required to achieve the target residual moisture content. Uniform drying is particularly important for solid dosage development because excessive moisture may cause sticking, poor flow, or instability, while over-drying can produce brittle granules or affect compaction behavior.
The air handling system forms an important part of the contained drying operation. Incoming and exhaust air must be managed so that the process receives suitable airflow while airborne material remains within the controlled system. Replaceable dual-layer HEPA filters, including PUSHPUSH-type arrangements, or bag-in/bag-out filter systems can be selected according to the containment strategy and maintenance requirements.
After drying, the granules can be discharged through a flip-valve arrangement or a vacuum discharge system. These options provide flexibility for different material behaviors and process layouts. The selection may depend on the required discharge direction, the available space, the bulk density of the dried product, and the desired connection to downstream equipment.
The dried material then proceeds through the dry granulation stage. Dry granulation is useful when a formulation requires further densification, improved flow, or size control without the addition of more liquid. It can also be used where the material is sensitive to moisture or heat. Combining wet granulation and dry granulation capabilities in one high-containment line gives development teams more process flexibility than a system limited to a single granulation method.
In a development setting, this flexibility can be valuable during formulation screening. Different materials may respond better to alternative granulation routes. A contained line allows the development team to compare processing conditions while keeping the same general containment architecture.
Once the granules have been processed, they are conveyed to the mixing hopper. The hopper provides a controlled location for final blending, lubricant addition, excipient incorporation, or other formulation steps required before compression or encapsulation.
After mixing is complete, the hopper outlet is connected to AB valves for final discharge. The finished granules leave the isolator through the AB valve while the containment boundary remains protected. This arrangement is designed to avoid open product transfer and can support connection to a downstream container, packaging system, tablet press, capsule-filling machine, or other receiving equipment.
Controlled discharge is one of the most important parts of a potent-product process. A line may perform well during granulation and drying, yet still create a significant risk if the final product must be manually emptied into an open container. The GFH process route maintains containment through the final transfer interface, helping provide a consistent protection strategy from beginning to end.
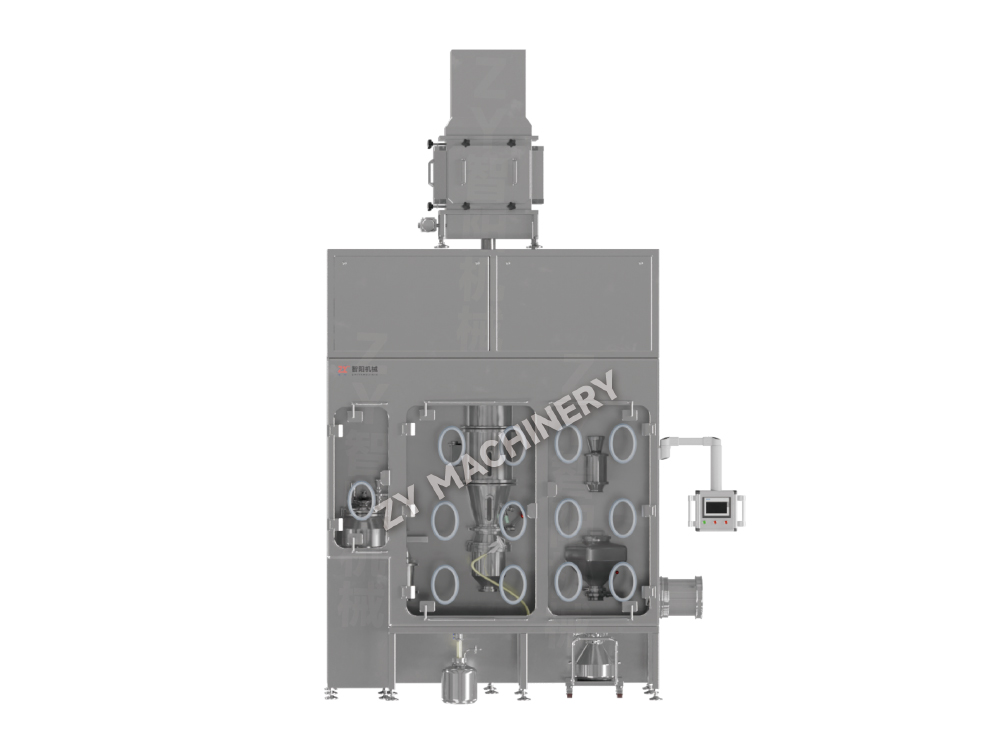
GFH R&D High-Containment Solid Dosage Production Line
The central advantage of the system is its isolator-based containment architecture. The isolator encloses the main processing equipment and provides a controlled working environment for high-potency materials. It is intended to support OEB4/OEB5 protection levels, subject to the final system design, operating procedures, validation, and site-specific performance verification.
The isolator can be configured with different access and manipulation methods. Glove ports allow operators to perform selected tasks without opening the enclosure. Half-suits may be used when greater access or more extensive manipulation is required. Robotic systems can be considered for applications where minimizing direct operator interaction is a priority.
This configurable approach is an important distinction compared with fixed, one-format containment systems. Development laboratories often handle several formulations and equipment configurations. A system that supports different glove-port layouts, half-suit arrangements, and automation levels can be matched more closely to the actual process risk and operating frequency.
During normal operation, the operating cabin pressure is specified within a range of approximately -50 Pa to -150 Pa. Negative pressure helps ensure that air moves into the isolator rather than outward into the surrounding room if minor leakage occurs. The airflow mode is identified as turbulent, and the ventilation frequency is specified as more than 15 air changes per hour.
Airflow performance must be evaluated together with filter efficiency, enclosure integrity, glove-port design, door sealing, transfer procedures, and the characteristics of the processed material. A negative-pressure value by itself does not define the complete containment performance. The benefit of the GFH design is that these elements are considered as part of an integrated system.
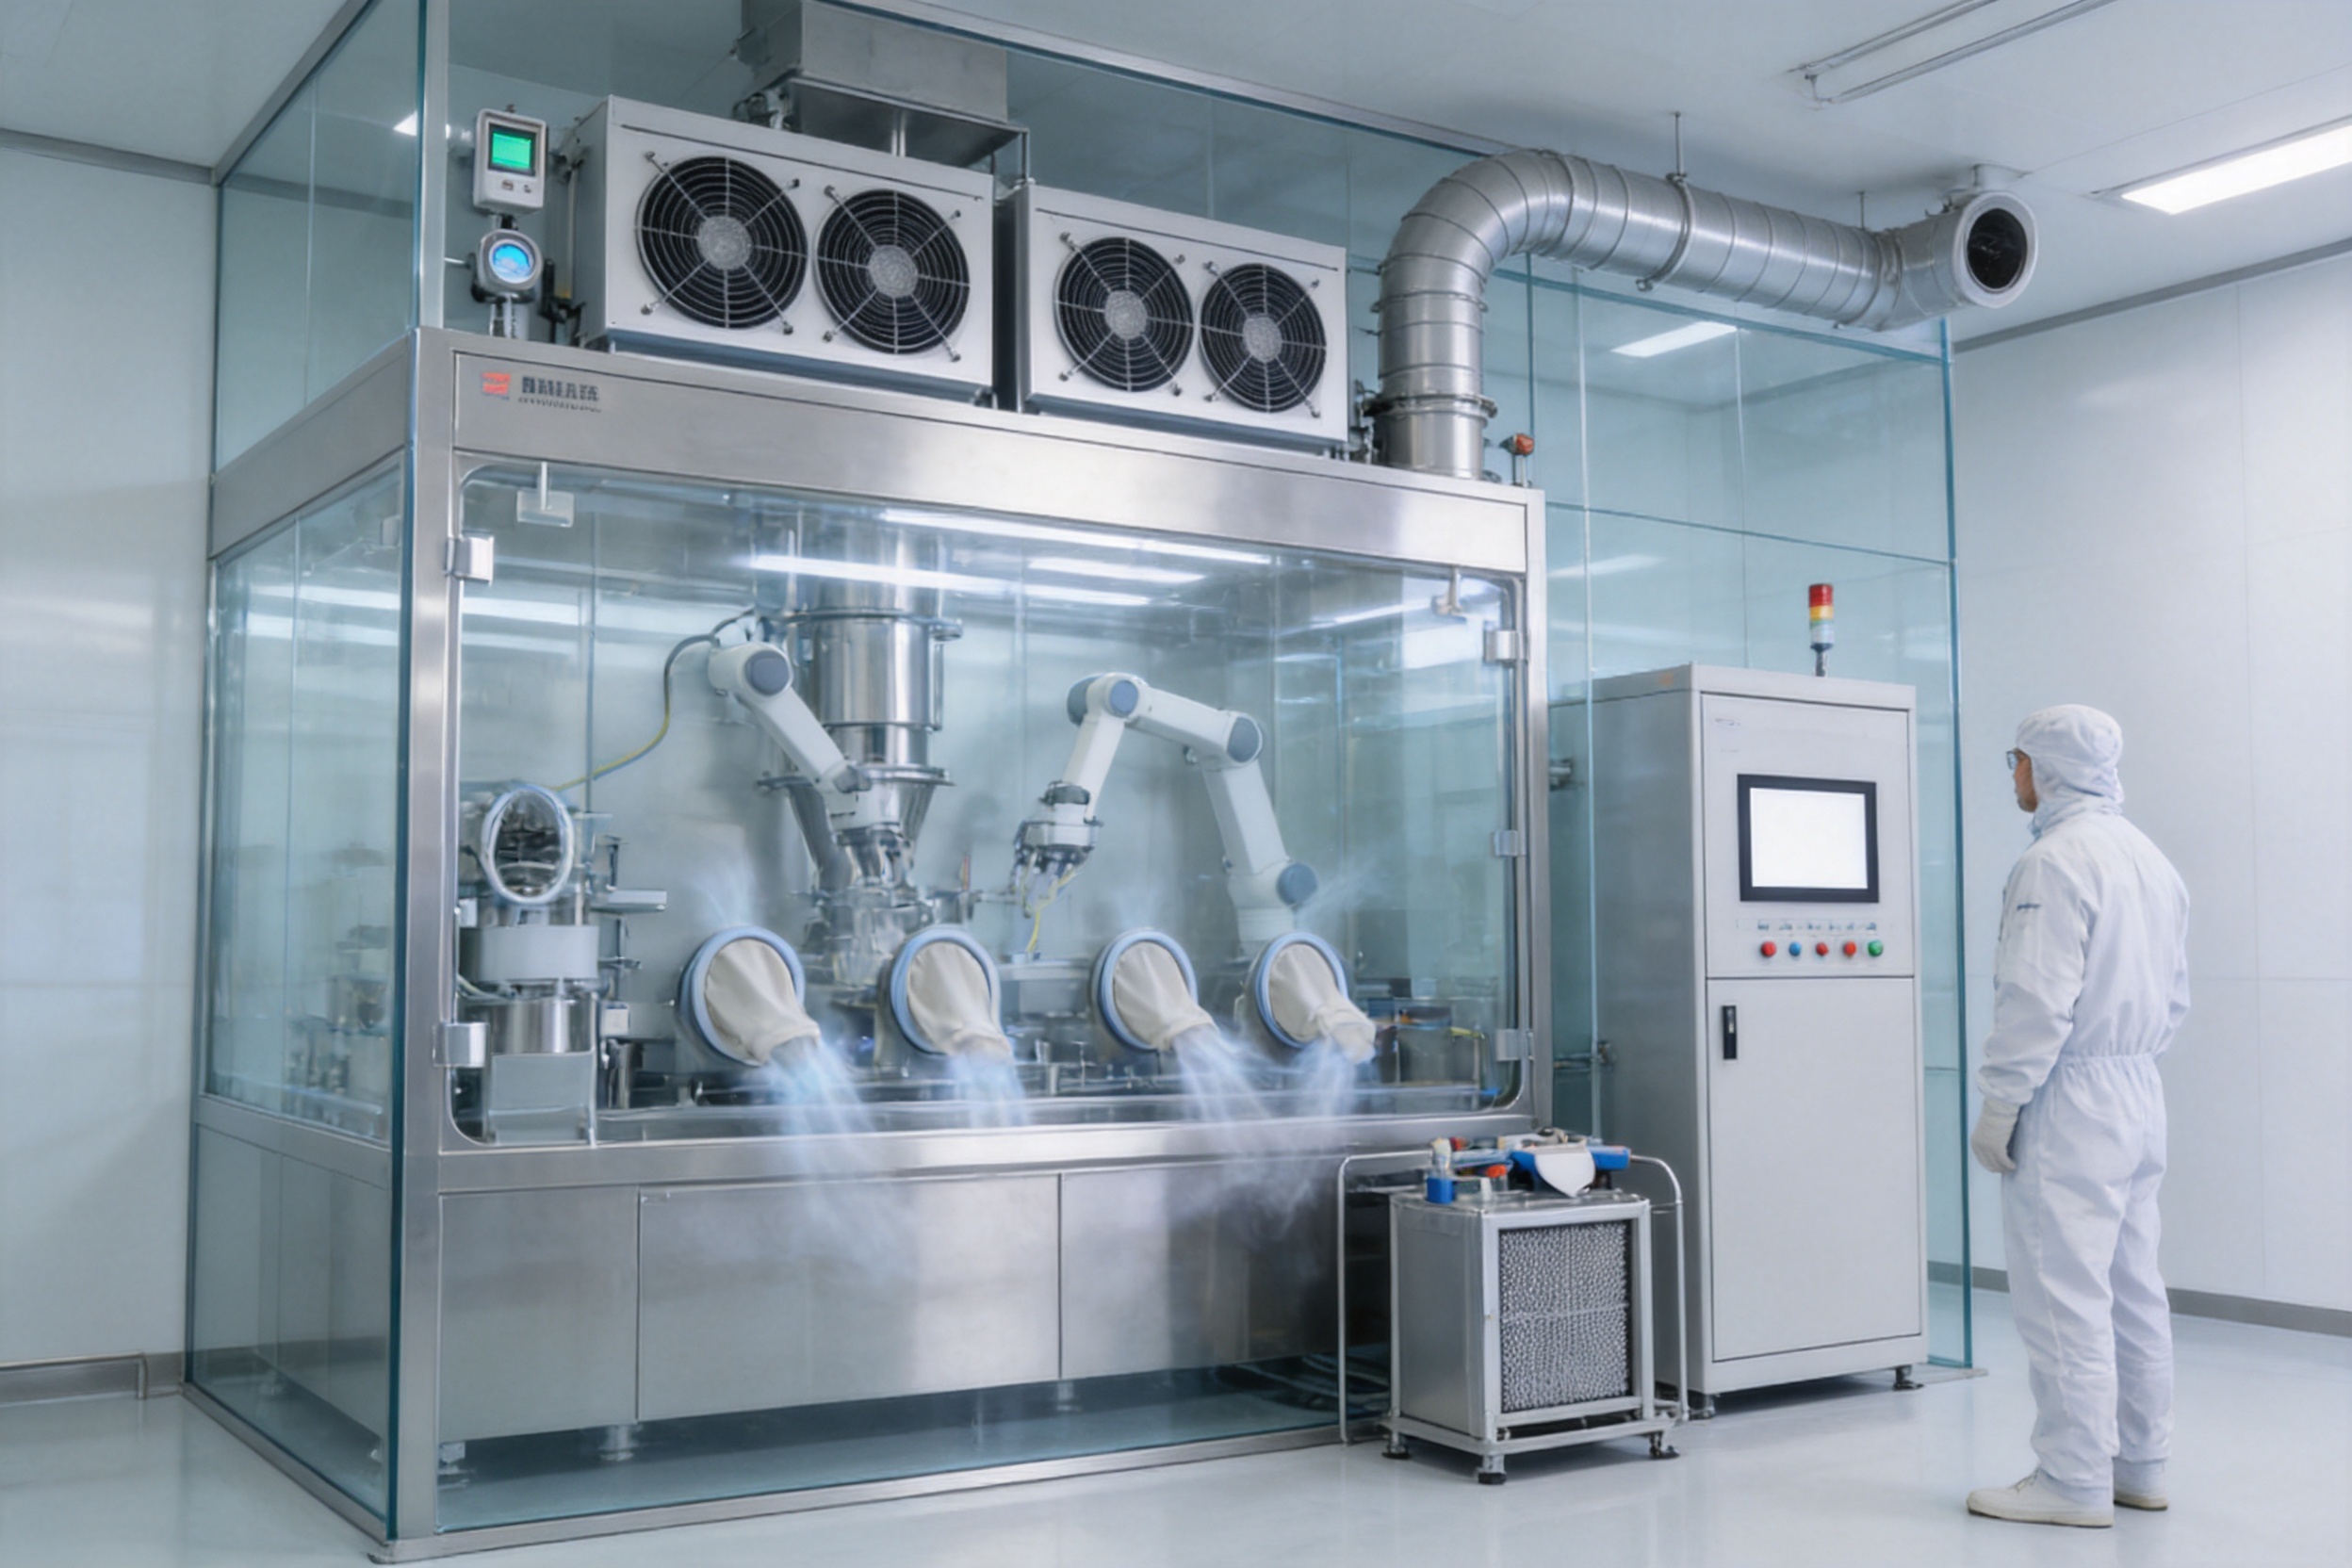
High-containment equipment must be designed for abnormal conditions as well as routine production. The GFH system includes an emergency mode intended to respond to events such as glove rupture or seal failure. In an emergency, the system rapidly increases internal pressure, activates alarms, adjusts fan speed, maximizes exhaust, and closes air inlets.
The emergency strategy is intended to maintain airflow above 0.5 m/s and reduce the possibility of high-potency material escaping from the isolator. The control response provides operators with an immediate indication of the fault and supports a defined intervention procedure. The exact emergency sequence should be reviewed, tested, and documented during commissioning and qualification.
This automated response provides an important advantage over basic enclosures that depend entirely on manual recognition of a failure. A rapid, coordinated response can reduce the time between fault detection and containment stabilization. It can also help standardize the reaction to an incident across different operating shifts.
Gloves are essential interfaces between the operator and the enclosed process. At the same time, they are potential points of weakness if damaged, improperly installed, or degraded by chemicals, abrasion, heat, or repeated movement. The system can include online glove integrity testing to support routine verification.
Safe glove replacement is also available as an optional feature. A replacement procedure should be designed so that the damaged glove can be removed and the new glove installed without unnecessarily exposing the operator or the surrounding environment. The final procedure depends on the glove material, port design, product hazard, cleaning status, and site operating instructions.
Air handling is a major factor in both containment and process performance. The system can use replaceable dual-layer HEPA filters in a PUSHPUSH configuration or bag-in/bag-out filters. These options allow the filtration arrangement to be selected according to the plant’s maintenance philosophy, available utilities, filter-change strategy, and containment requirements.
Dual-layer filtration provides an additional barrier for exhaust air and can support safer filter replacement planning. Bag-in/bag-out systems are widely used when contaminated filters must be removed and replaced without direct exposure to the surrounding environment. The most appropriate arrangement depends on the product hazard assessment and the site’s standard operating procedures.
Filter replacement is not simply a maintenance task. It is a critical containment operation that should be controlled through suitable bags, clamps, seals, tools, and documented procedures. The equipment design can be paired with accessory systems for bag handling and sealing to help make this operation more predictable.
The air handling system also influences drying efficiency. Fluidized-bed drying requires suitable airflow, temperature control, and exhaust management. The process must balance drying performance with the need to retain fine particles and prevent contamination of downstream or external areas. An integrated air handling design makes it easier to coordinate these requirements.
Material transfer is often the most challenging part of high-containment production. Every transfer introduces a connection, opening, seal, or movement between process stages. The GFH line supports multiple transfer approaches, including RTPs, transfer chambers, and sleeve systems.
RTP technology is suitable when a standardized rapid connection is preferred. Transfer chambers can provide an intermediate controlled space for moving materials, tools, or components. Sleeve systems may be useful where flexible connection and bag handling are required. Interlocked doors provide an additional safeguard by controlling access to the transfer chamber.
The selection of a transfer method should consider the form of the material, the batch size, the frequency of transfer, the cleaning strategy, the required level of automation, and whether the receiving equipment is inside or outside the isolator. Because the line is customizable, the transfer strategy can be developed around the customer’s process rather than forcing the process to conform to a fixed layout.
Contained transfer also improves material accountability. When the process is closed and the transfer points are defined, it is easier to identify where material enters, where it is processed, and where it leaves. This can support batch documentation, reconciliation, cleaning verification, and deviation investigation.
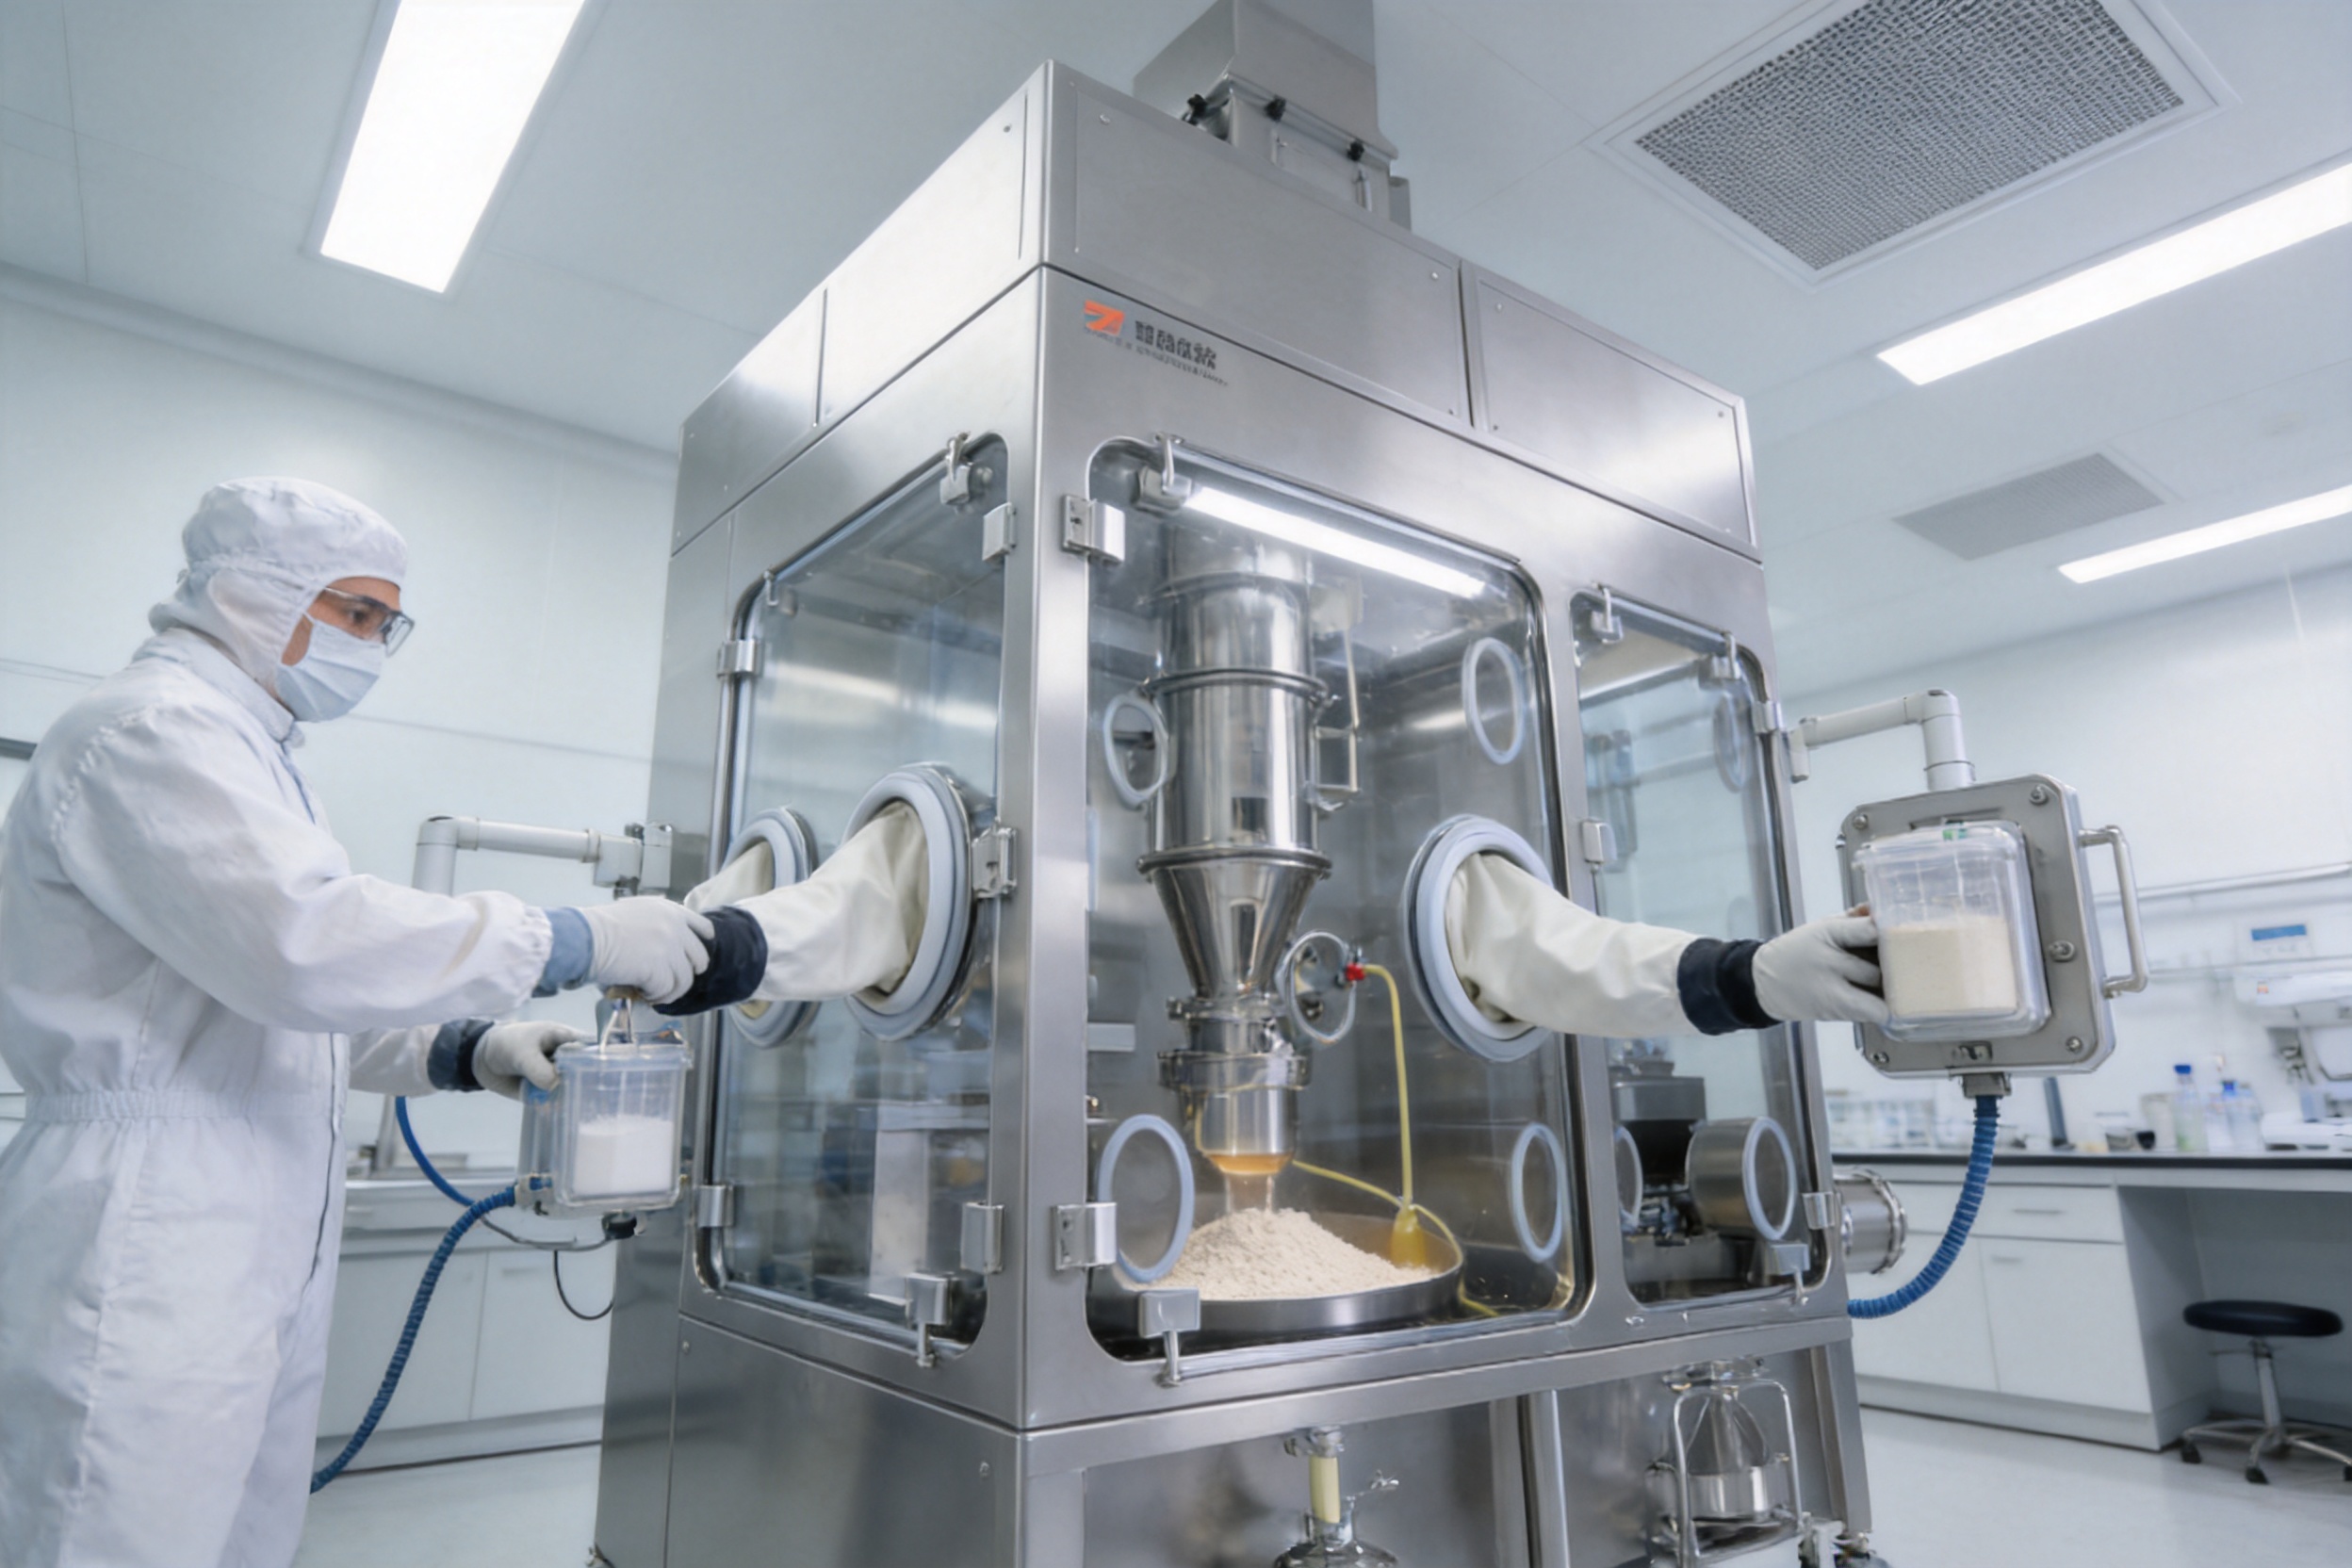
The GFH line uses a logic controller-operated system with a user-friendly human-machine interface. A centralized control architecture allows operators to monitor and manage the principal process stages from a common interface. Depending on the final configuration, controlled functions may include transfer sequencing, granulation operation, vacuum conveying, drying parameters, fan speed, pressure monitoring, alarm handling, and discharge coordination.
Centralized control is advantageous because high-containment processing involves multiple interdependent functions. For example, a transfer door should not open when the corresponding process condition is unsafe. A discharge valve may need to remain closed until the receiving container is correctly connected. An emergency event may require simultaneous changes to fans, inlets, exhaust, alarms, and access conditions.
Logic-based interlocks help make these relationships consistent. They can reduce reliance on memory and support repeatable operation across batches. The HMI can also provide status information, alarm notifications, operating prompts, and process records, subject to the selected automation and documentation package.
Repeatability is especially important during research and development. Scientists need to compare formulations and process conditions without introducing unnecessary variability from manual transfers or inconsistent equipment operation. A controlled sequence can improve the reliability of experimental results.
Repeatable control also supports scale-up decisions. Data obtained from a contained development line can help identify the impact of granulation time, drying conditions, transfer behavior, and blending performance before a larger production system is selected. The equipment does not replace formal process development, but it provides a practical platform for generating meaningful process knowledge.
Containment equipment should provide clear indication of abnormal pressure, filter, glove, door, airflow, or transfer conditions. The HMI-based control structure can be configured to present alarms in a logical manner and guide the operator toward an approved response.
Alarm design should distinguish between warnings, process interruptions, and emergency conditions. It should also prevent unauthorized bypassing of safety functions. Final alarm limits, access permissions, data recording, and user management should be defined during the engineering and qualification phases.
The GFH range is available in several nominal batch capacities. The listed models cover approximately 1 kg, 3 kg, 5 kg, 10 kg, and 20 kg per batch. This range is suited to laboratory investigation, formulation development, pilot work, and selected small-scale production applications.
| Parameter | Unit | GFH-1 | GFH-3 | GFLH-5 | GFLH-10 | GFLH-20 |
| Capacity | kg/batch | 1 | 3 | 5 | 10 | 20 |
| Total power | kW | 6.2 | 8.15 | 6.9 | 10.65 | According to design |
| Electrical heater power | kW | 4.5 | 4.5 | 4.5 | 9 | According to design |
| Protection level | — | OEB4/OEB5 | OEB4/OEB5 | OEB4/OEB5 | OEB4/OEB5 | OEB4/OEB5 |
| Airflow mode | — | Turbulent | Turbulent | Turbulent | Turbulent | Turbulent |
| Ventilation frequency | air changes/hour | More than 15 | More than 15 | More than 15 | More than 15 | More than 15 |
| Operating cabin pressure | Pa | -50 to -150 | -50 to -150 | -50 to -150 | -50 to -150 | -50 to -150 |
| Compressed-air consumption | m³/h | 0.2 | 0.3 | 0.6 | 0.9 | According to design |
| Compressed-air pressure | MPa | 0.4 to 0.6 | 0.4 to 0.6 | 0.4 to 0.6 | 0.4 to 0.6 | 0.4 to 0.6 |
| External dimensions | mm | According to design | According to design | According to design | According to design | According to design |
| Machine weight | kg | According to design | According to design | According to design | According to design | According to design |
The values in the table are reference parameters. Actual power, dimensions, weight, air consumption, heating configuration, and equipment arrangement may vary according to the selected process route, utility conditions, material characteristics, and site layout. The 20 kg configuration in particular should be confirmed during technical design because larger batch sizes may require different heating, conveying, filtration, and structural arrangements.
The GFH line offers several practical advantages when compared with conventional open processing or systems assembled from disconnected equipment modules.
A primary advantage is the continuation of containment across wet granulation, drying, dry granulation, mixing, and discharge. In a conventional arrangement, operators may need to manually empty one machine and load another. Each open transfer increases the possibility of dust release, operator exposure, product loss, and cross-contamination.
By combining the equipment inside an isolator and using controlled transfer methods, the system reduces the number of open handling steps. This can make it easier to establish a consistent containment strategy and simplify the training required for operators.
Many competing systems are optimized for a single process or a narrow batch range. The GFH line provides a broader development route by including wet granulation, fluidized-bed drying, dry granulation, mixing, and multiple discharge options. This makes it possible to evaluate different process sequences using one principal containment platform.
Such flexibility is valuable for pharmaceutical developers working with new chemical entities, highly potent compounds, specialized excipients, or formulations that have not yet been fully characterized. The system can accommodate process learning instead of requiring the final manufacturing route to be known from the beginning.
The availability of glove ports, half-suits, and robotic options allows the containment interface to be matched to the task. Some operations may require frequent manual intervention, while others may be suitable for automated handling. A flexible access concept can improve ergonomics and help balance containment performance with productivity.
The emergency mode is another differentiating feature. Rather than treating glove rupture or seal failure as an event managed solely through manual action, the system uses automated pressure, airflow, exhaust, inlet, and alarm responses. This integrated response can reduce reaction time and provide a more predictable safety procedure.
Optional glove integrity testing, safe glove replacement, and bag-in/bag-out filtration support the ongoing maintenance of the containment boundary. These features are important because high-containment performance must be sustained throughout the equipment lifecycle, not only during initial production.
The equipment is designed according to batch capacity, material characteristics, process requirements, and site conditions. This process-driven approach can be more effective than selecting a standard machine and attempting to adapt the production process afterward. A properly engineered line can use available room dimensions, utilities, transfer paths, and downstream connections more efficiently.
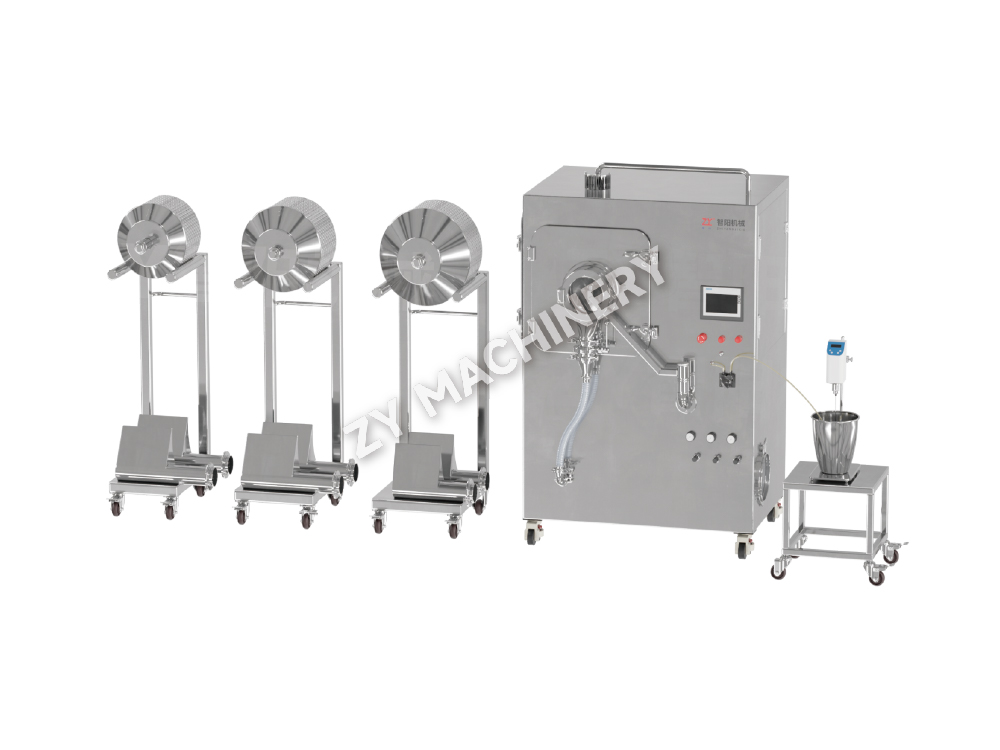
Changzhou Zhiyang Machinery Equipment Co., Ltd. specializes in powder processing and oral solid dosage equipment. Its product scope covers laboratory equipment, mixing equipment, granulation equipment, drying equipment, coating equipment, auxiliary processing equipment, and transfer and conveying systems. This broad range is relevant to high-containment projects because a complete line often requires several equipment categories to work together.
The company’s engineering approach is based on process integration rather than the supply of isolated machines. It develops solutions according to material properties, capacity requirements, and customer site conditions. This allows the design team to consider the entire route, including charging, containment, granulation, drying, transfer, blending, discharge, cleaning, maintenance, and future expansion.
Founded in 2010 and based in Changzhou, China, the company serves pharmaceutical, biopharmaceutical, biotechnology, nutraceutical, veterinary, additives, and related industries. Its experience across these sectors supports an understanding of different powder behaviors, production objectives, and equipment integration requirements.
Powder processing equipment cannot be selected effectively by capacity alone. Particle size, bulk density, flowability, cohesiveness, moisture sensitivity, electrostatic behavior, heat sensitivity, and cleaning requirements all influence the correct configuration. The company’s process-oriented method considers these factors when preparing equipment and engineering proposals.
For a high-containment line, the design process must also address the hazard classification, containment target, transfer technology, filter arrangement, glove strategy, door sealing, emergency response, and maintenance concept. A process-based engineering review helps ensure that these elements work together rather than being added independently at a later stage.
The manufacturer supplies standalone machines, modular systems, and complete production lines. This gives customers several project options. A laboratory may begin with a contained granulation and drying configuration, while a larger development center may require a complete line with transfer, mixing, and final discharge. The modular approach can allow the system to evolve as the product and process mature.
Complete line integration can also reduce coordination challenges. When one engineering partner is responsible for the principal process route, it may be easier to define interfaces, utility requirements, control logic, safety interlocks, and documentation responsibilities.
The company has expanded its product portfolio, strengthened research and development capabilities, developed patented technologies, and obtained quality system certification. These resources support the ongoing improvement of equipment design and process functionality.
Research and development capability is particularly important for high-containment systems because customer requirements are often highly specific. The ideal arrangement may depend on a compound’s potency, the intended batch size, the desired cleaning method, the required degree of automation, and the number of products processed in the same facility.
Equipment and engineering solutions have been delivered to customers in multiple countries and regions. Overseas project experience can help the manufacturer understand differences in plant layouts, utility standards, documentation expectations, installation procedures, and service requirements.
For customers purchasing specialized containment equipment, responsive technical communication is important. A successful project requires more than fabrication. It involves process discussions, layout review, factory testing, installation support, commissioning, operator training, and after-sales service.
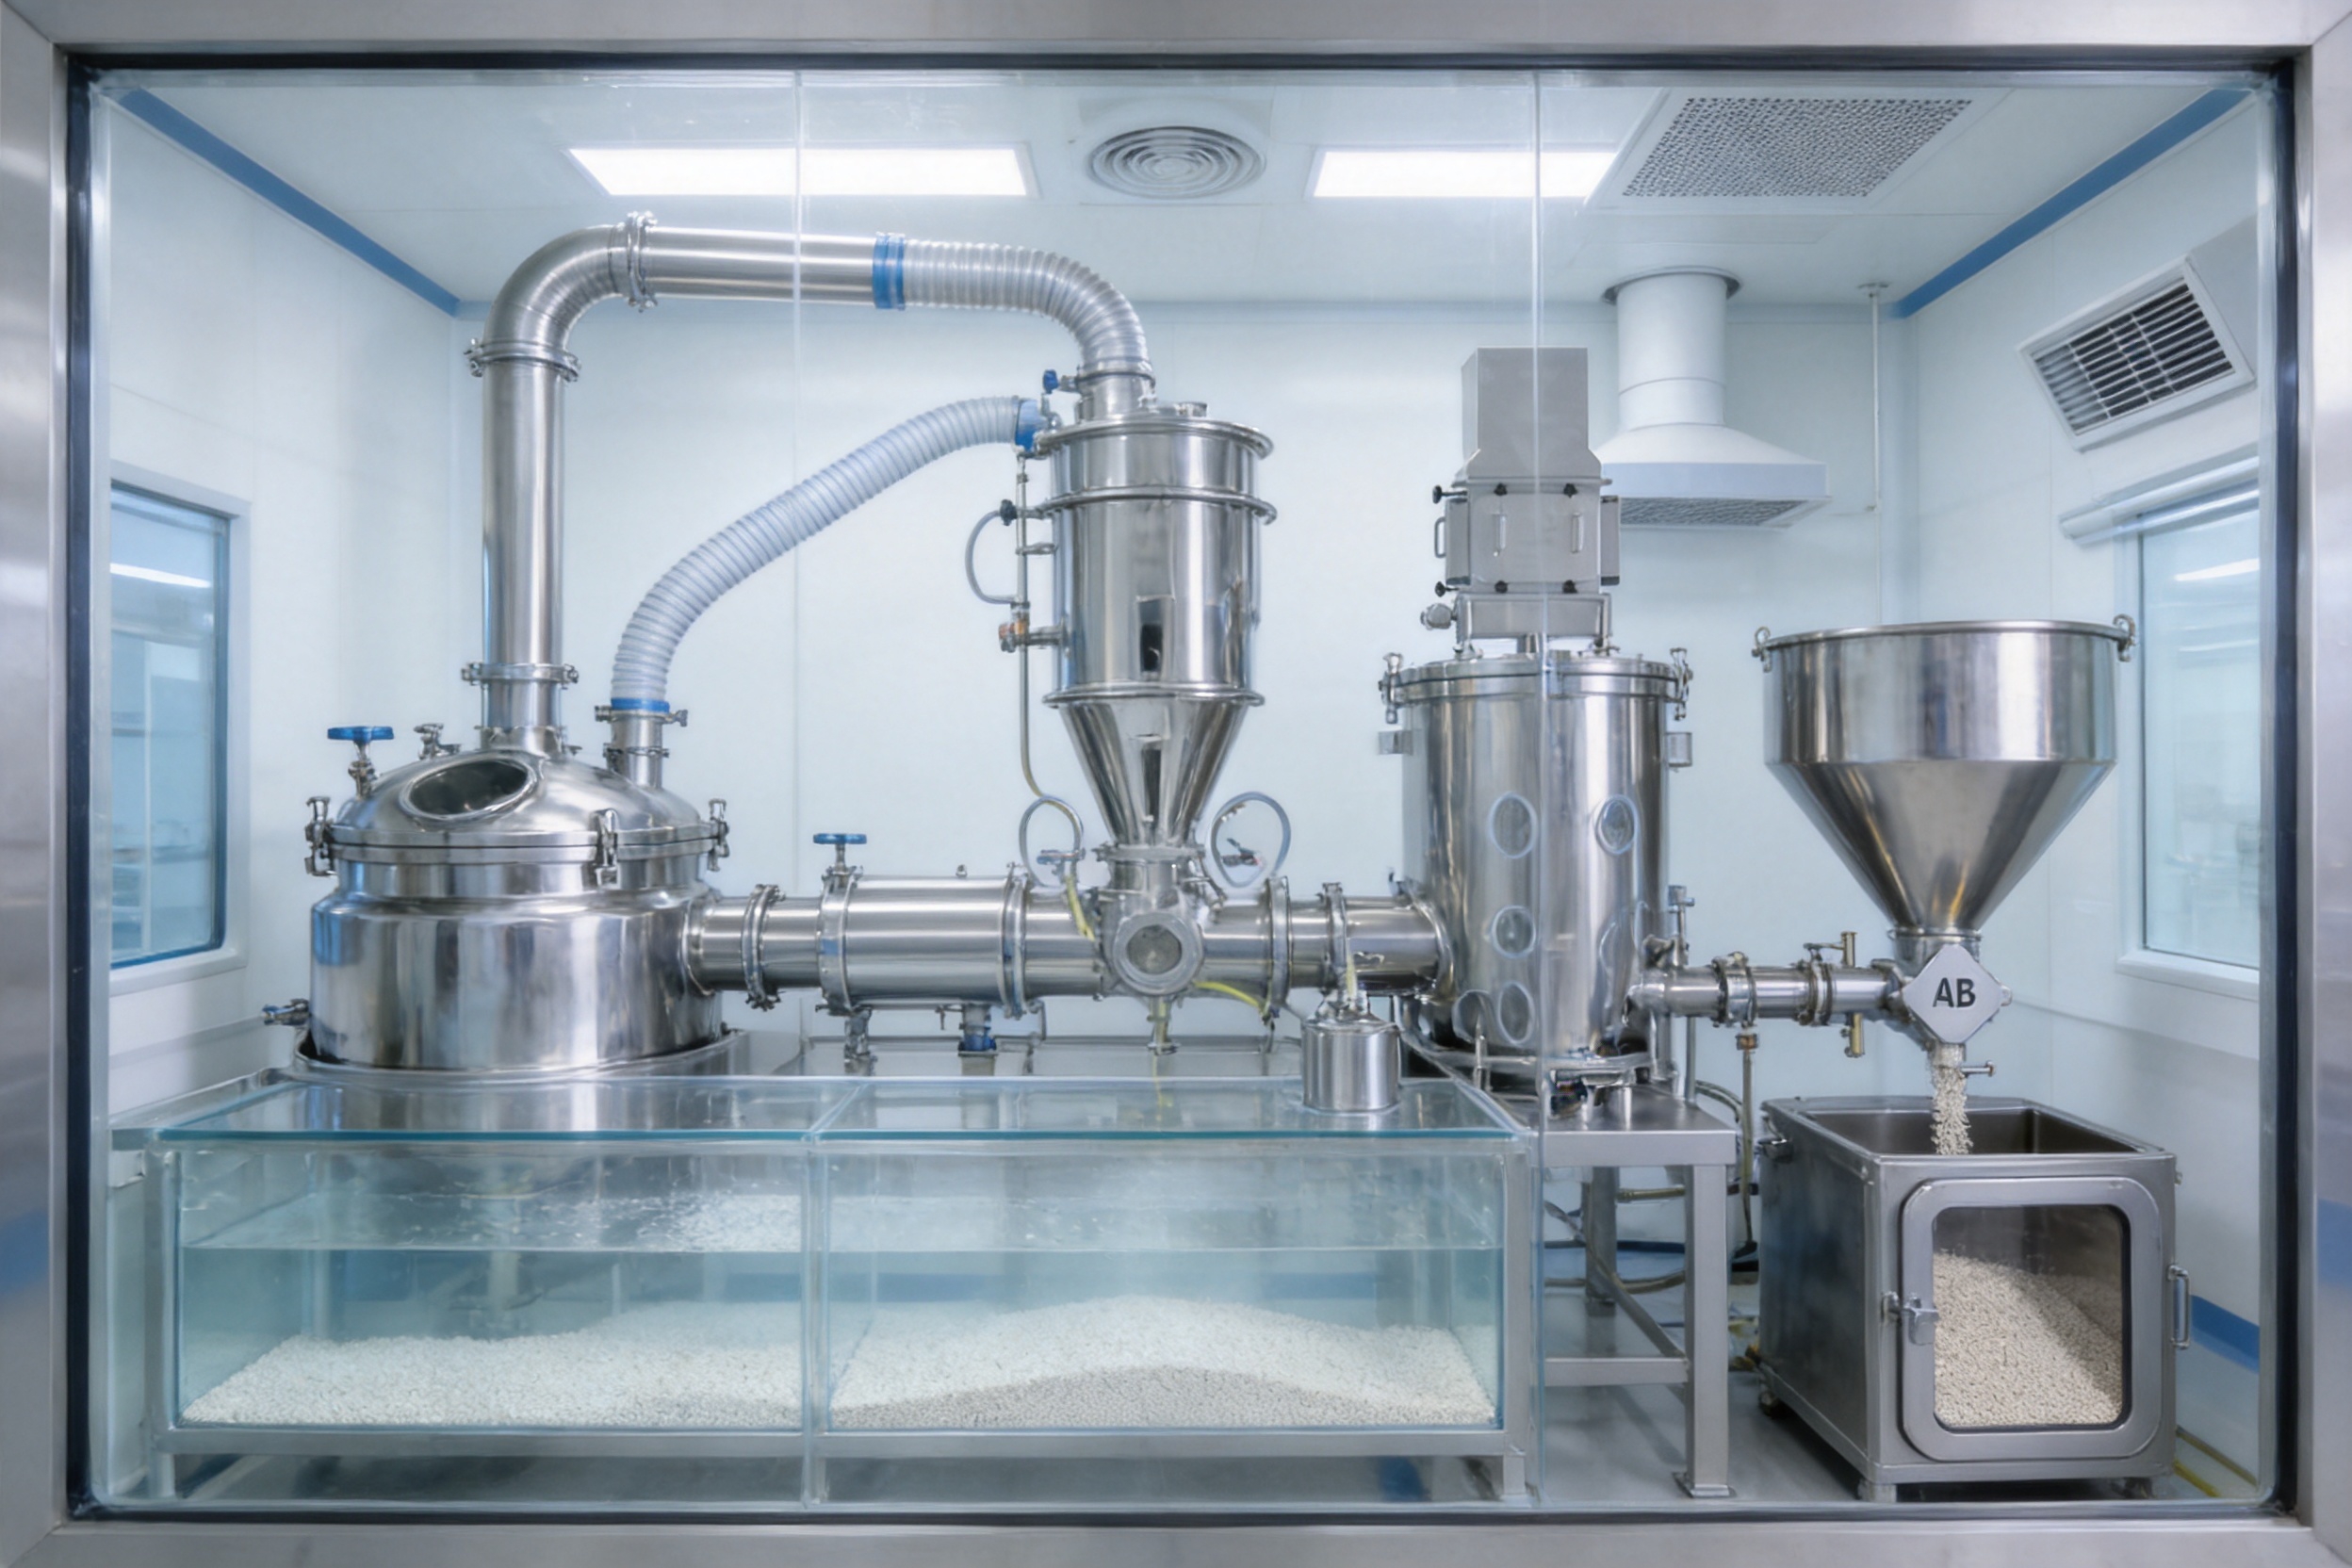
Before selecting a high-containment solid dosage line, buyers should define the intended materials, batch sizes, process route, containment objective, and future production plans. A clear user requirement specification can help prevent costly changes after fabrication begins.
The equipment configuration should reflect the behavior of the actual powder or granule. Important characteristics include particle-size distribution, moisture content, bulk density, flowability, cohesiveness, abrasiveness, electrostatic tendency, and sensitivity to temperature or shear.
Materials that bridge, cake, smear, or become electrostatically charged may require specialized transfer or discharge designs. Materials with a narrow moisture specification may require enhanced drying control. Highly cohesive powders may need particular attention to vacuum conveying and hopper geometry.
The nominal capacity should be matched to the expected working volume rather than the maximum theoretical volume. Development batches may vary significantly depending on the formulation and experimental objective. The selected model should provide sufficient operating flexibility for under-filled and full-batch conditions.
Customers should also consider whether the line will support scale-up studies. A system that provides consistent process control and documented operating parameters can generate more useful information for later commercial equipment selection.
Cleaning strategy is a central part of potent-product equipment design. Buyers should determine whether the process will use manual cleaning, contained wet cleaning, dry cleaning, or a combination of methods. Contact surfaces, seals, glove ports, valves, filters, transfer hoses, and product containers should all be included in the cleaning assessment.
Changeover time, disassembly requirements, accessibility, and cleaning verification should be reviewed before finalizing the layout. A system that is difficult to clean may reduce availability and increase the risk of carryover, even if its process performance is otherwise satisfactory.
OEB4/OEB5 is a target protection level, not a substitute for site-specific testing. Customers should establish the required performance tests for enclosure integrity, airflow, pressure stability, filter installation, glove integrity, transfer interfaces, and emergency response.
Containment performance may be assessed through appropriate industrial hygiene and engineering methods. Test protocols should be agreed upon during the design stage so that the equipment is prepared for commissioning, qualification, and routine verification.
The equipment requires suitable electrical power, compressed air, ventilation connections, and floor space. Compressed-air pressure is specified at approximately 0.4 to 0.6 MPa, while consumption varies by model and final configuration. Actual utility requirements should be confirmed using the approved equipment design.
Facility planning should include access for delivery, installation, maintenance, filter replacement, component removal, and emergency response. The layout should also consider personnel flow, material flow, waste removal, and the relationship between the isolator and surrounding rooms.
The system can be supplied with accessory options intended to support contained operation and maintenance. A polyethylene bag handling kit can assist with the controlled management of bags used for material transfer, waste collection, filter handling, or component protection.
Sealing clamps can provide a controlled method for closing flexible bags and sleeves. Packaging tools may support the final handling of finished granules or the connection of product containers. The appropriate accessory package depends on the product form, transfer method, batch size, and customer procedures.
Accessories should be treated as part of the containment concept rather than as optional conveniences. A well-designed bag, clamp, or packaging interface can reduce the number of improvised handling steps and make routine operations safer and more repeatable.
The GFH line is suitable for research and development involving potent oral solid dosage products. Typical applications include the preparation of granules for tablet compression, capsule filling, formulation screening, process parameter development, and pilot-scale manufacturing.
It may be used for anticancer compounds, highly sensitizing materials, and other potent substances where operator protection is a major design requirement. The system can also support development programs in which the active ingredient is scarce or expensive, because enclosed transfer may reduce material loss during handling.
For nutraceutical, veterinary, biotechnology, and specialty additive applications, the same contained process concepts may be useful when powders create occupational, environmental, or cross-contamination concerns. The final suitability of the equipment must be evaluated according to the specific material hazard and regulatory requirements.
During formulation screening, developers may need to compare binder systems, granulation endpoints, drying conditions, and blending sequences. An integrated line allows these experiments to be performed with fewer manual transfers. This can improve the consistency of comparisons between trial batches.
Once a formulation has been selected, the line can support optimization of wet granulation, drying, dry granulation, and final mixing conditions. Operators can evaluate the relationship between process parameters and granule properties such as flowability, density, moisture, particle size, and compressibility.
The available capacities provide a bridge between laboratory-scale experimentation and larger manufacturing systems. The exact production rate depends on the formulation, cycle time, equipment configuration, and operating method. Nevertheless, a contained pilot platform can help identify practical issues before a full-scale investment is made.
A high-containment line should be implemented through a structured engineering process. The initial stage normally includes a review of the user requirement specification, material properties, batch sizes, process sequence, containment target, layout, utilities, cleaning method, and automation expectations.
Design review should verify that all critical interfaces are addressed. These include RTP connections, chamber doors, glove ports, half-suit openings, filters, flexible sleeves, valves, hoses, electrical controls, and emergency systems. The final arrangement should be evaluated for both normal operation and maintenance activities.
Factory acceptance testing can be used to review mechanical assembly, control logic, alarms, interlocks, airflow functions, pressure response, transfer interfaces, and documentation before shipment. Site acceptance and commissioning then confirm the equipment’s performance after installation in the customer’s facility.
Qualification activities should be based on the customer’s quality system and applicable regulatory expectations. They may include installation qualification, operational qualification, performance verification, containment testing, filter integrity testing, glove integrity testing, airflow assessment, and process trials.
Training is also essential. Operators should understand material charging, transfer procedures, glove-port use, alarm response, emergency mode, discharge, cleaning, waste handling, and personal protective equipment requirements. Maintenance personnel require additional training for filters, seals, valves, fans, sensors, and control components.
Changzhou Zhiyang Machinery Equipment Co., Ltd. provides engineering and service support for equipment projects, including process planning, system integration, installation assistance, and overseas service capabilities. The value of this support lies in helping the customer convert a machine purchase into a functioning production solution.
For potent solid dosage processing, the lowest purchase price does not necessarily represent the lowest total cost. A system that requires extensive manual transfer, complex cleaning, repeated operator intervention, or frequent containment repairs may create higher operating costs over its lifecycle.
An integrated line can reduce the number of separate interfaces, simplify material movement, and support more consistent production. It may also reduce the need for additional rooms, temporary transfer equipment, or manual containment measures. These benefits should be evaluated together with capacity, installation cost, validation requirements, maintenance, energy use, and future expansion.
The GFH system combines several important capabilities: high-containment isolation, configurable operator access, controlled air handling, multiple transfer options, wet and dry granulation, fluidized-bed drying, mixing, final discharge, and centralized control. This combination makes it a practical option for organizations that need to develop or produce potent solid dosage products without sacrificing process flexibility.
Its strongest competitive advantage is not a single component. It is the coordination of the complete process route. The system is designed to keep hazardous materials enclosed while moving through several operations that would otherwise require repeated open handling. This integrated design can improve safety, product consistency, and operational efficiency.
The line is intended for solid dosage development and production, including tablets, capsules, and granules. It is especially suitable for highly potent or hazardous materials such as anticancer drugs and highly sensitizing compounds.
The system is designed to provide OEB4/OEB5 protection levels. Actual performance depends on the final configuration, operating procedures, maintenance condition, material properties, and verification testing carried out at the customer’s site.
Materials are transferred through an RTP valve. Depending on the project, transfer chambers and sleeve systems may also be incorporated. Interlocked chamber doors can be used to improve transfer safety.
Wet granules are vacuum-transferred to a fluidized-bed drying unit. After drying, the product can be discharged through a flip-valve or vacuum discharge system and then processed through the dry granulation stage.
Yes. The process route includes wet granulation followed by drying and dry granulation. This provides development flexibility for formulations that require densification, improved flow, or additional size control.
After mixing in the hopper, the outlet is connected to AB valves. Finished granules leave the isolator through the AB valve, helping maintain containment during final discharge.
The isolator can be customized with different glove-port arrangements, half-suits, or robotic systems. The appropriate option depends on the type and frequency of operator intervention required.
When a glove rupture or seal failure is detected, the system can increase internal pressure, trigger alarms, adjust fan speed, maximize exhaust, and close air inlets. The emergency strategy is intended to maintain airflow above 0.5 m/s and help prevent the escape of potent materials.
Online glove integrity testing is available as an optional feature. Safe glove replacement can also be included to support maintenance while reducing exposure risk.
The air handling system can use replaceable dual-layer HEPA filters, including PUSHPUSH-type designs, or bag-in/bag-out filters. The preferred option should be selected according to the containment strategy and site maintenance procedures.
Reference models include capacities of approximately 1 kg, 3 kg, 5 kg, 10 kg, and 20 kg per batch. Final working capacity should be confirmed according to the formulation, bulk density, equipment configuration, and process requirements.
Yes. External dimensions, machine weight, power, heating capacity, and utility consumption are determined according to the final design. Site conditions and process layout are considered during engineering.
It is suitable for laboratory, research, development, pilot, and selected small-batch production applications. The controlled process route can help generate data for later scale-up, although larger commercial systems should be designed and validated separately.
Customers should review material properties, containment targets, batch capacity, process route, cleaning method, transfer technology, filter replacement strategy, utility requirements, automation level, room layout, downstream connections, and qualification expectations.
The GFH R&D High-Containment Solid Dosage Production Line provides an integrated solution for the controlled processing of highly potent pharmaceutical powders and granules. By combining an isolator with RTP transfer, wet granulation, vacuum conveying, fluidized-bed drying, dry granulation, mixing, and AB-valve discharge, the system is designed to maintain containment throughout the main solid dosage process.
Its configurable glove ports, half-suits, robotic options, filtration systems, transfer chambers, sealing methods, glove testing, and emergency response functions allow the line to be tailored to different risk profiles and operating methods. The available batch capacities make it appropriate for formulation development, pilot work, and selected small-scale production.
The manufacturer’s strengths extend beyond equipment fabrication. Its experience in powder processing, oral solid dosage equipment, process integration, customized engineering, modular system design, research and development, and international service enables customers to develop a complete project rather than purchase unrelated machines.
For organizations working with anticancer drugs, highly sensitizing substances, or other hazardous solid dosage materials, the most important requirement is a reliable and coherent containment strategy. An integrated system such as the GFH line can help reduce manual exposure points, support consistent process control, and create a practical foundation for safer pharmaceutical development and production.
1. International Society for Pharmaceutical Engineering. Good Practice Guide: Assessing and Managing the Risks of Occupational Exposure to Hazardous Drugs and Pharmaceutical Compounds.
2. United States Pharmacopeia. General guidance related to pharmaceutical manufacturing, powder handling, and solid dosage quality.
3. European Medicines Agency. Principles and expectations for the manufacture and control of pharmaceutical products.
4. International Society for Pharmaceutical Engineering. Pharmaceutical Engineering Baseline Guides for facilities, equipment, and containment.
5. World Health Organization. Good manufacturing practices for pharmaceutical products.
6. Relevant industrial hygiene guidance concerning occupational exposure bands, high-potency active pharmaceutical ingredients, and engineering containment controls.
7. Manufacturer-provided technical information for the GFH R&D High-Containment Solid Dosage Production Line, including process description, configuration options, and reference parameters.
Want to stay up to date?
Contact us via the email address below.
Don't worry about spam. We hate it too!
Mobile Client
Video Account
Phone:+86-15161130178
Tel:+86-519-88674267
Email:czzy188@163.com
Phone:+86-15161132798
Email:zy@zy-drying.com
WeChat ID
Copyright 2026 Changzhou Zhiyang Machinery Equipment Co., Ltd. All Rights Reserved  Oral Solid Dosage Equipment Manufacturer